Leave Your Message
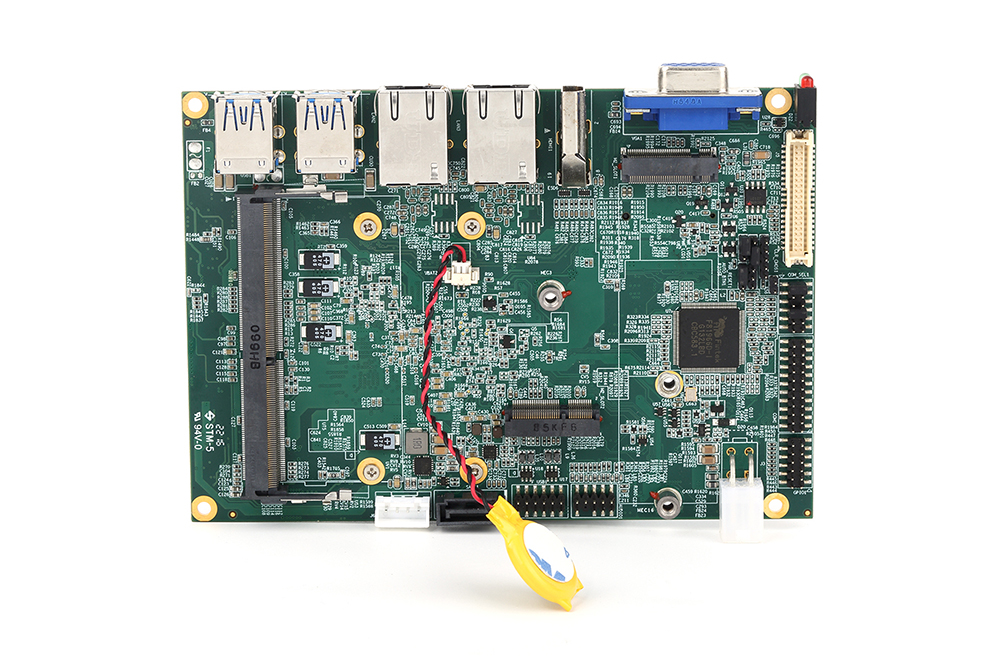
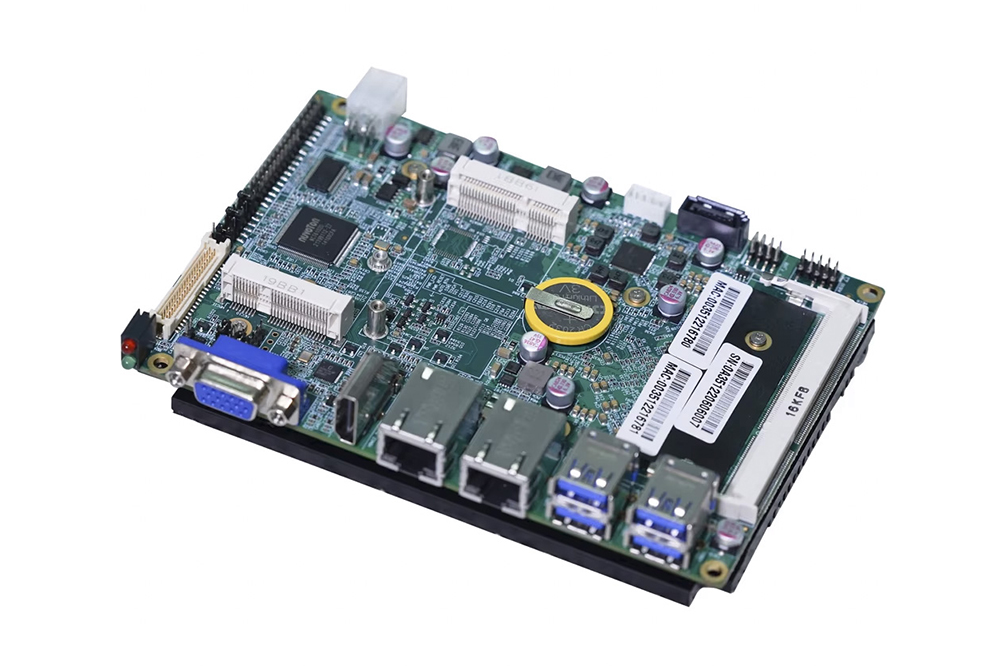
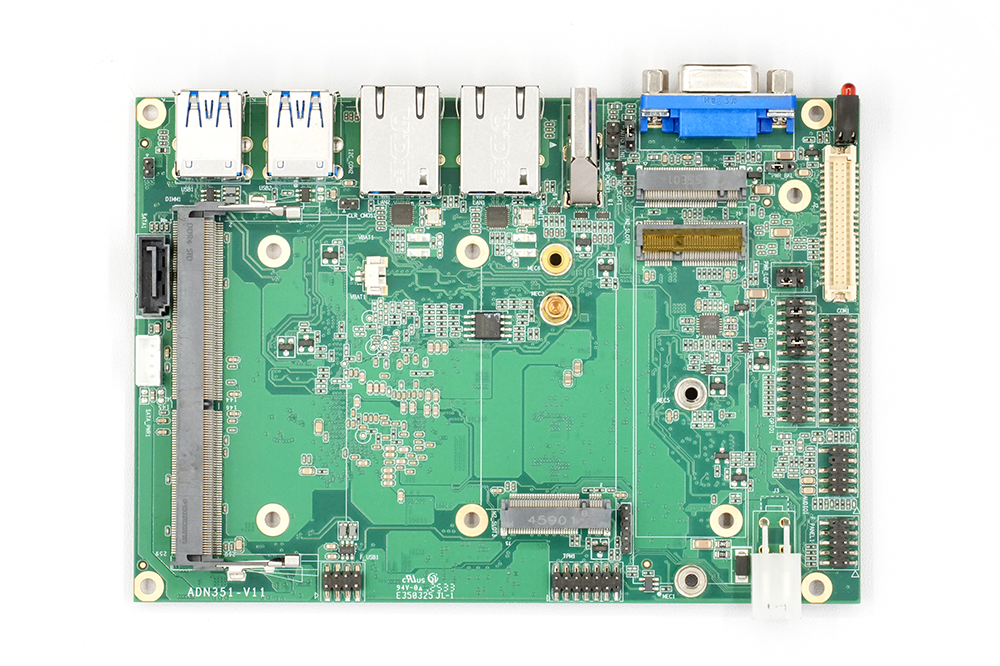
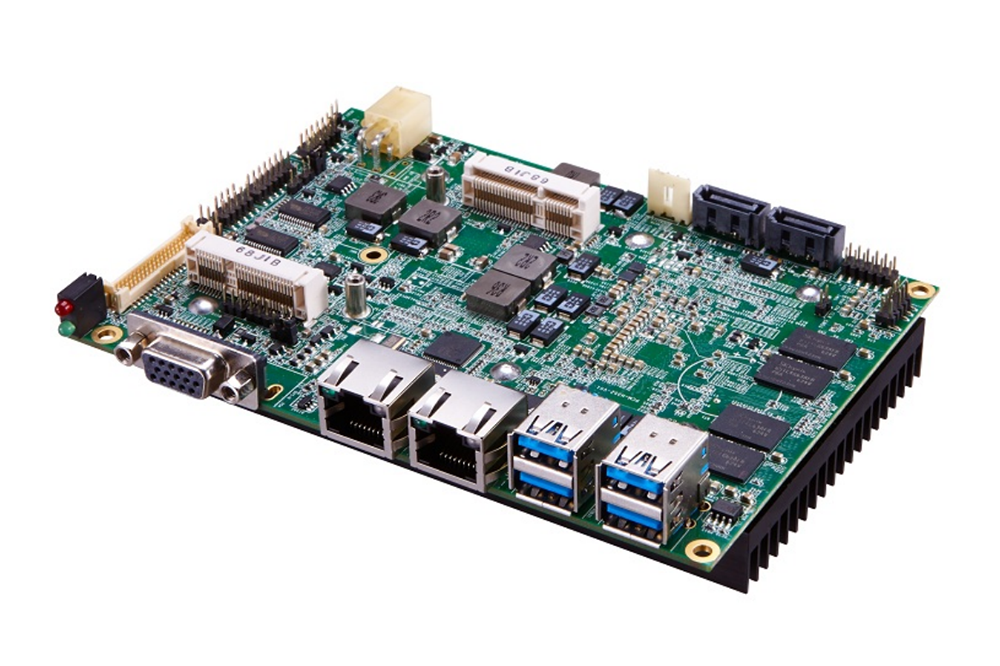
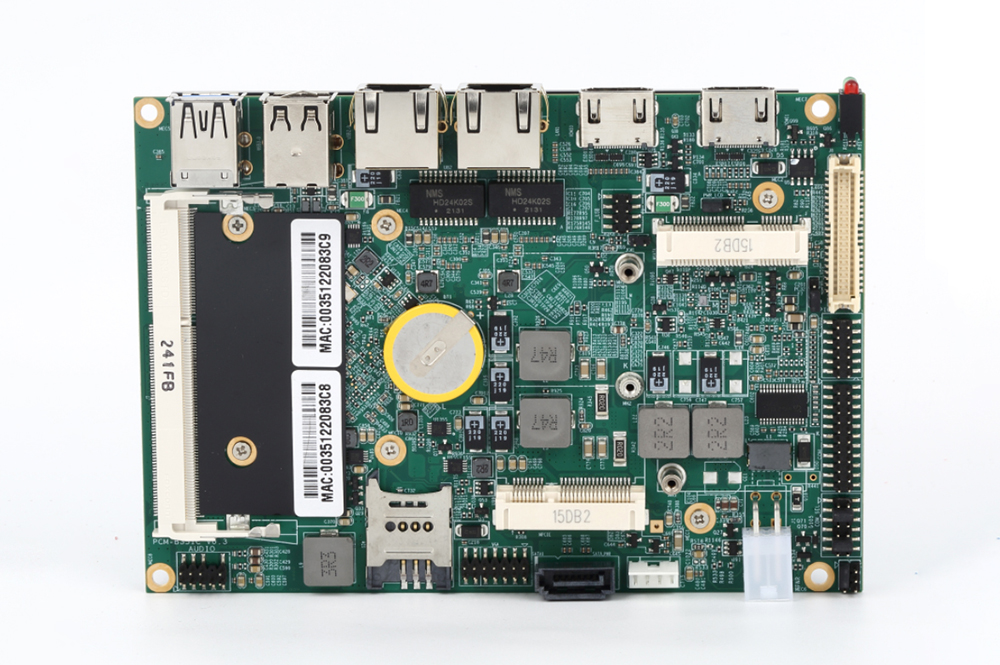
The United States stands as the global epicenter for medical device innovation, research, and manufacturing. Within this highly sophisticated industrial sector, the medical device motherboard serves as the fundamental digital core, powering everything from clinical diagnostic imaging suites to critical bedside ventilators. As healthcare systems across North America undergo rapid digital transformation, the demand for specialized, high-reliability embedded computing platforms has surged. These boards must meet rigorous regulatory standards, operate flawlessly in high-stress clinical settings, and support long lifecycles to align with hospital capital equipment timelines.
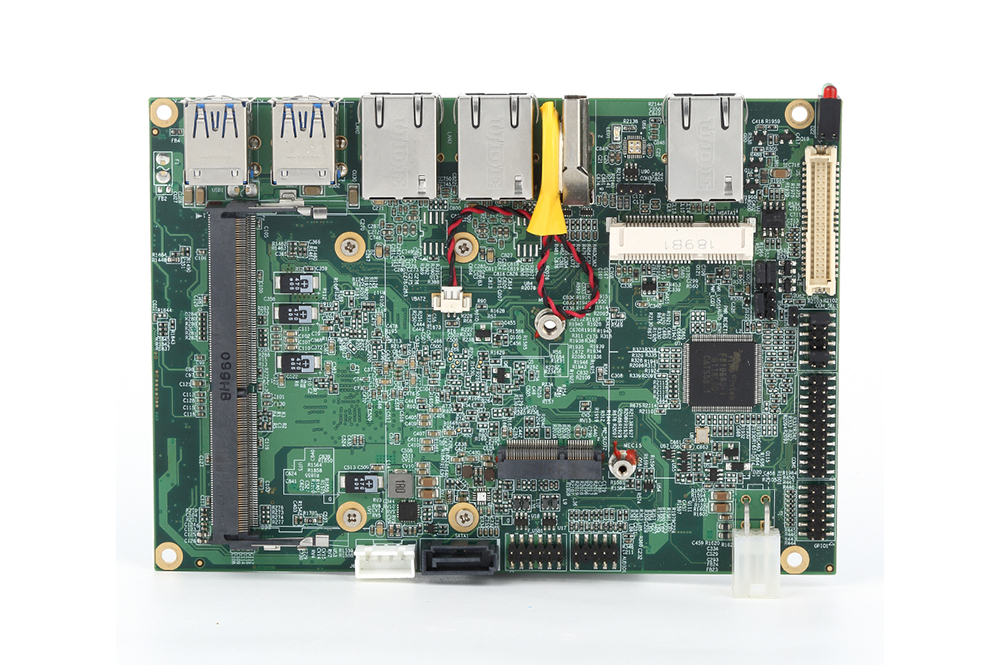
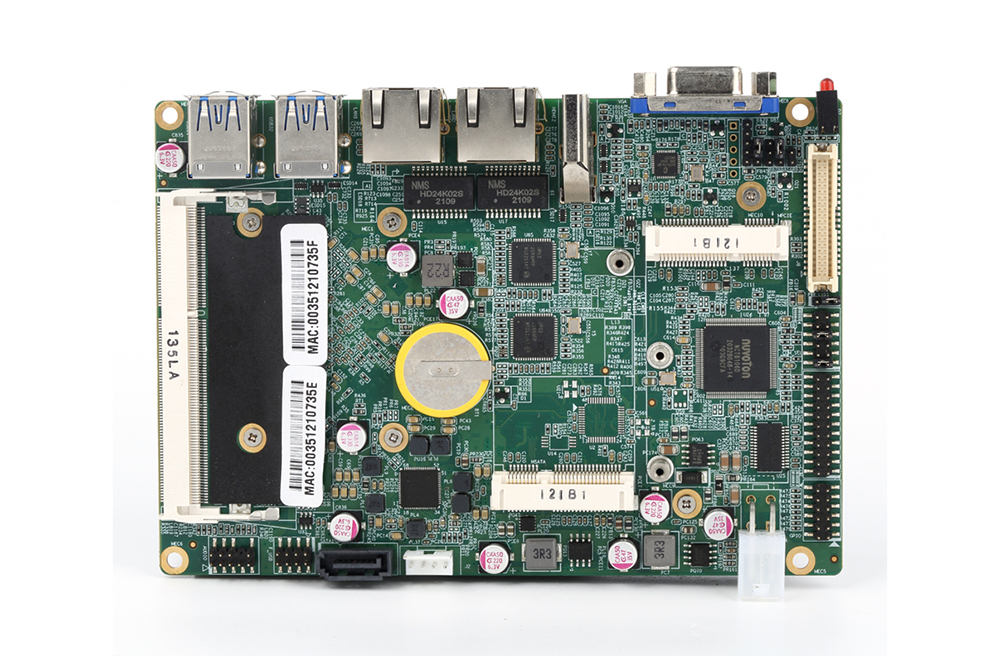
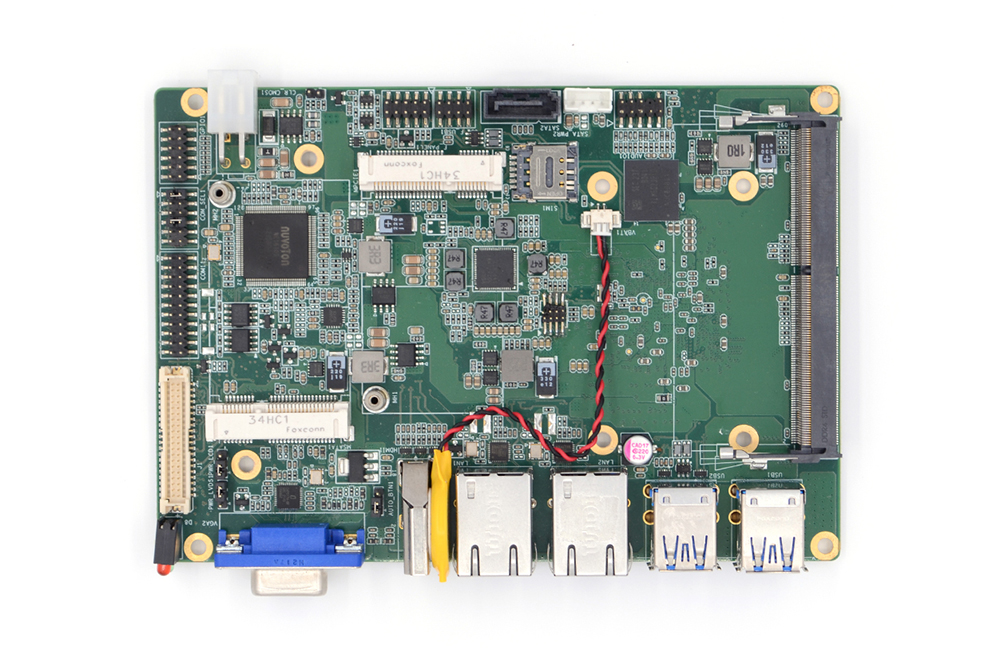
In the United States, commercial and industrial markets for medical motherboards are heavily shaped by the requirements of the Food and Drug Administration (FDA) and international safety standards such as IEC 60601-1. Unlike standard consumer hardware, a medical-grade motherboard must features advanced electromagnetic compatibility (EMC), galvanic isolation to protect patients and operators from electrical shocks, and fanless designs to minimize the spread of airborne contaminants in sterile environments. From Silicon Valley’s biotech startups to established medical conglomerates in Boston and Minneapolis, developers rely on robust x86 architectures to deliver deterministic performance for real-time patient data processing.
Engineered to assist developers in meeting strict FDA Class II and Class III medical equipment certification guidelines, offering low EMI emissions and high electrical isolation.
Product lifecycles guaranteed for up to 7-10 years, ensuring US medical OEMs avoid frequent, costly recertifications due to component obsolescence.
Balancing cutting-edge x86 processing power with optimized production costs, giving healthcare providers superior ROI for embedded IT infrastructure.
Several transformative trends are currently shaping the development and procurement of medical computer boards in the United States:
Embedded medical motherboards are deployed across a vast array of clinical and laboratory environments throughout the United States. Below are the primary application scenarios where these industrial-grade boards ensure operational continuity and patient safety:
In Intensive Care Units (ICUs) across major US hospital networks like the Mayo Clinic or Cleveland Clinic, reliability is a matter of life and death. Embedded motherboards power the central computing units of bedside monitors and ventilators, tracking heart rates, oxygen saturation, and respiratory metrics. The wide temperature support (ranging from -40°C to +85°C in premium models) ensures these devices boot instantly and run reliably, even in fluctuating environmental conditions or emergency transport vehicles.
From complex MRI and CT scan control consoles to portable ultrasound machines used in emergency rooms, medical motherboards process high-bandwidth imaging data. The integration of high-speed DDR4 memory and Intel-based architectures enables rapid image rendering and low-latency data throughput, helping radiologists make faster, more accurate diagnoses.
In-Vitro Diagnostics (IVD) and automated blood analyzers in reference labs (such as Quest Diagnostics or Labcorp) demand high-throughput processing and continuous operation. Industrial motherboards with rich serial communication ports (RS-232/422/485) and dual Gigabit LAN interfaces allow seamless control of robotic arms, fluid pumps, and sample barcode scanners while maintaining secure data transmission to the laboratory information system (LIS).
With the rise of rural telehealth initiatives and remote clinics in the US, ruggedized, fanless embedded PCs are deployed in public health kiosks. These systems allow patients to consult with specialists remotely, record vitals, and print prescription details. The fanless design ensures these kiosks remain low-maintenance and dust-resistant in public spaces.
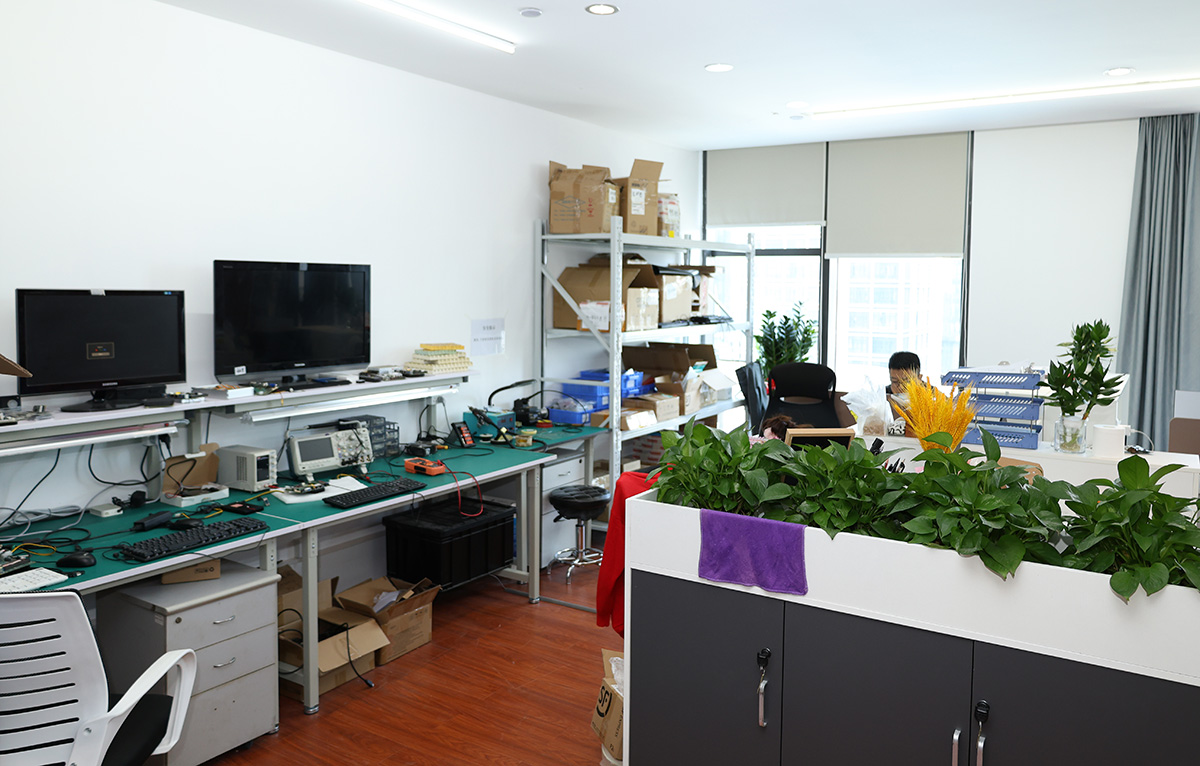
Shenzhen YDSTECH Electronics Co., Ltd. is a high-tech enterprise specializing in industrial computers. Since the establishment of YDSTECH in 1999, we have been committed to independent research and development, innovation, production and sales of industrial computers, and we own the independent intellectual property rights of our core products.
We consider honesty and pragmatism as our motto and make it our long-term goal to provide customers with cost-effective products. In order to achieve this goal, we work constantly to develop new products, improve our service capabilities and promote the innovation of embedded computer applications to create long-term value and potential growth for our customers.
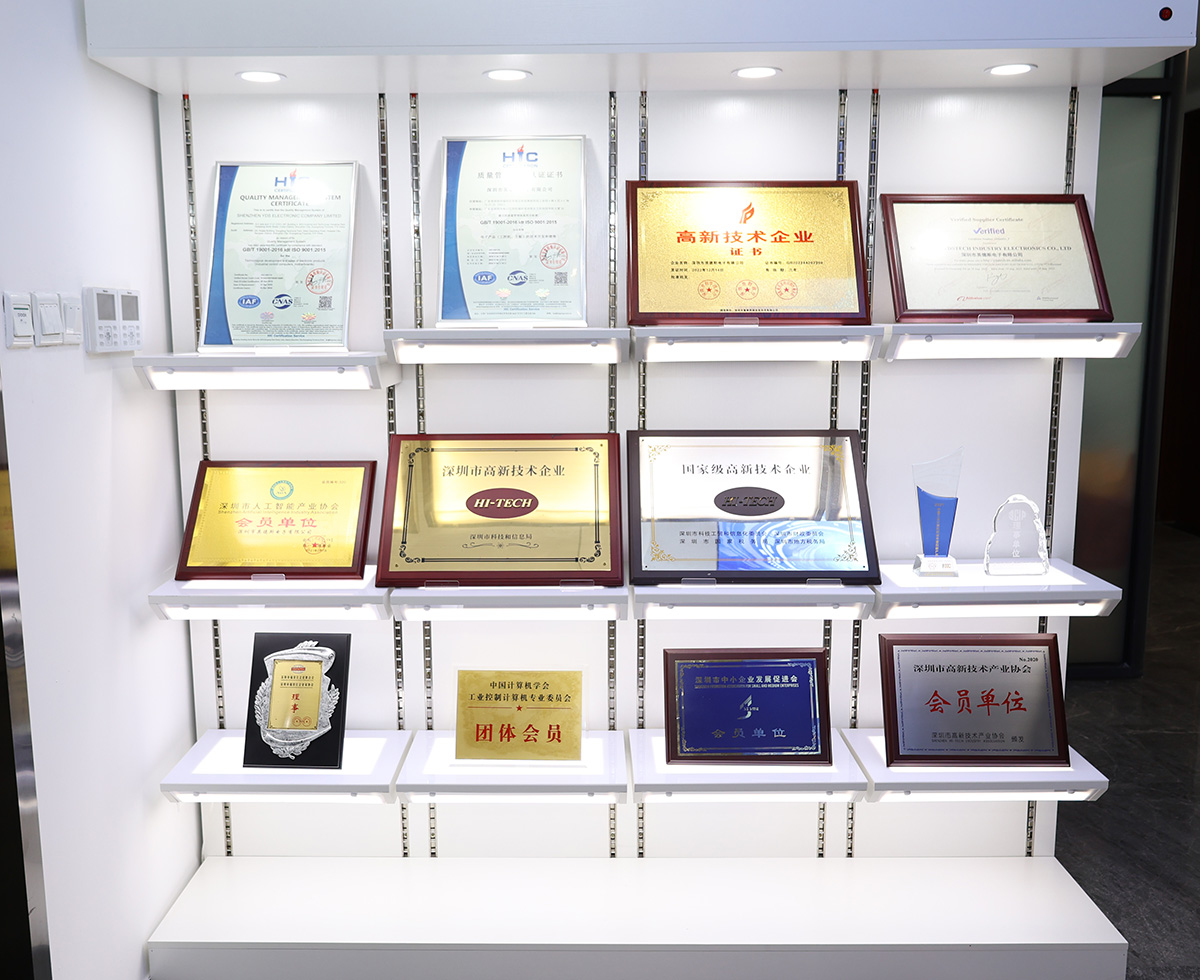
Our core technical team has over 15 years of experience in this industry, and has been focusing on embedded computer research and development, with rich and solid professional expertise. We believe that attitude means everything, since the establishment of YDSTECH, we have always been committed to work with a conscientious, responsible, attentive, professional, prudent and meticulous attitude, which ensures the high-quality output of the products, years of persistence and experience created our strong R&D team.
YDSTECH has set up a comprehensive quality assurance management system, adopting MSA quality system analysis, implementing rolling quality system audit, TQM, SPC process control and other quality management systems, establishing AVL supplier management system to ensure the quality of raw materials, and introducing rolling product reliability tests to ensure overall product reliability.