Leave Your Message
Explore our top-performing embedded boards designed to power rugged industrial PC screens and HMI interfaces across diverse American industries.
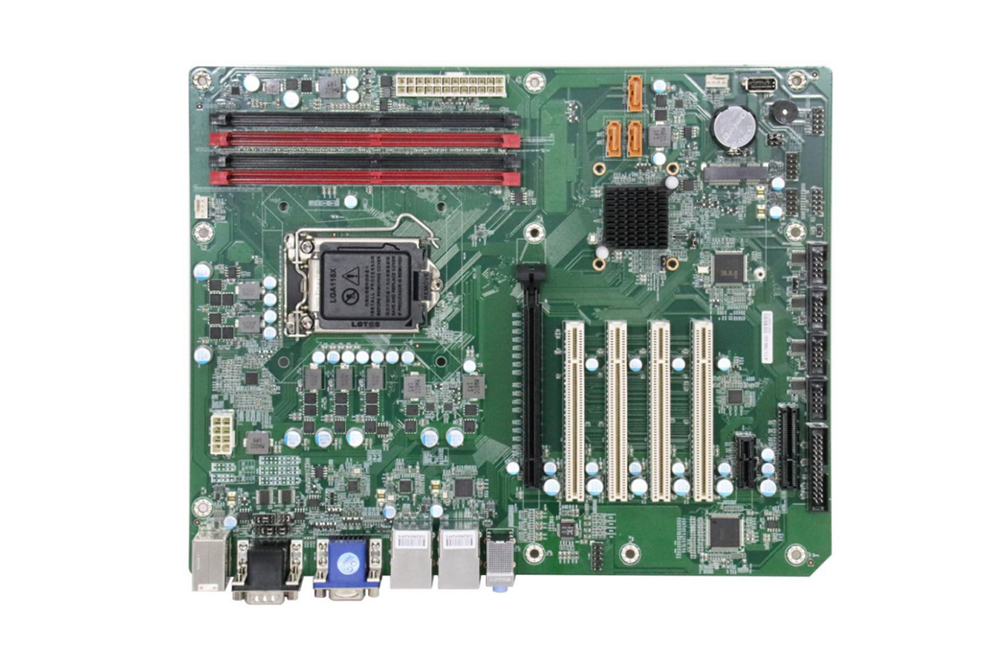
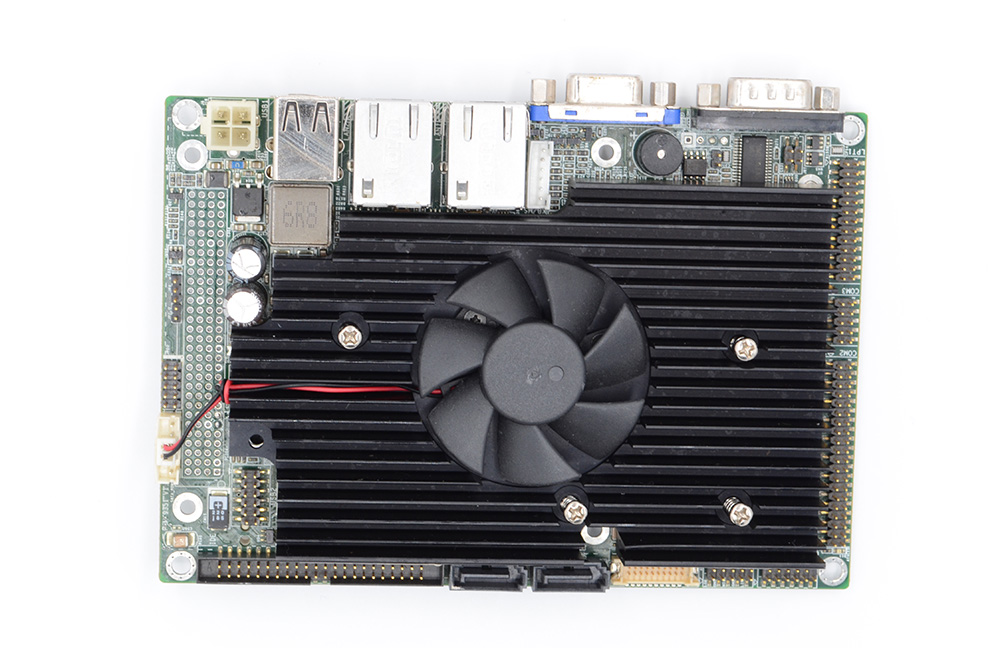
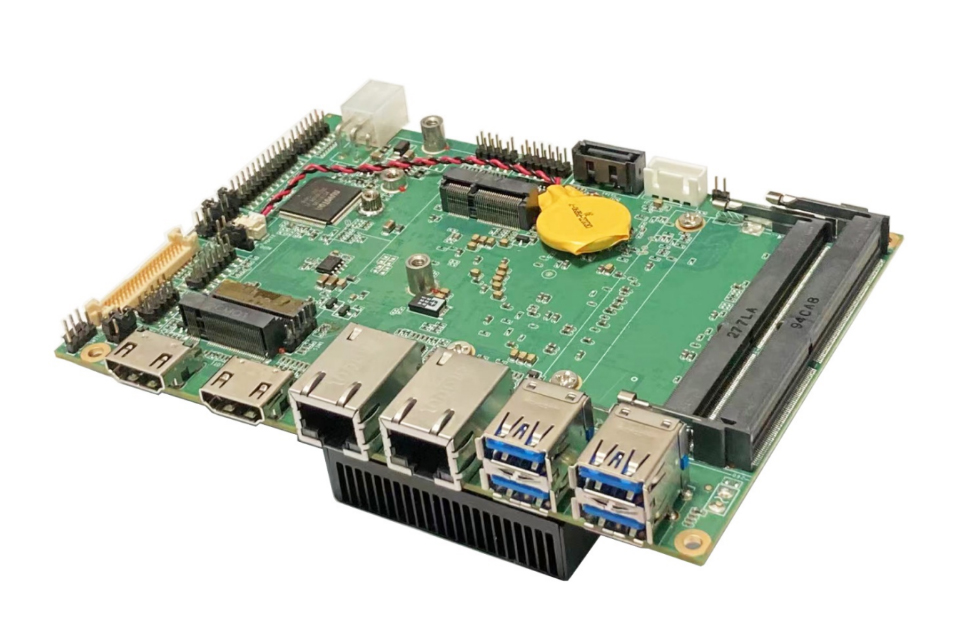
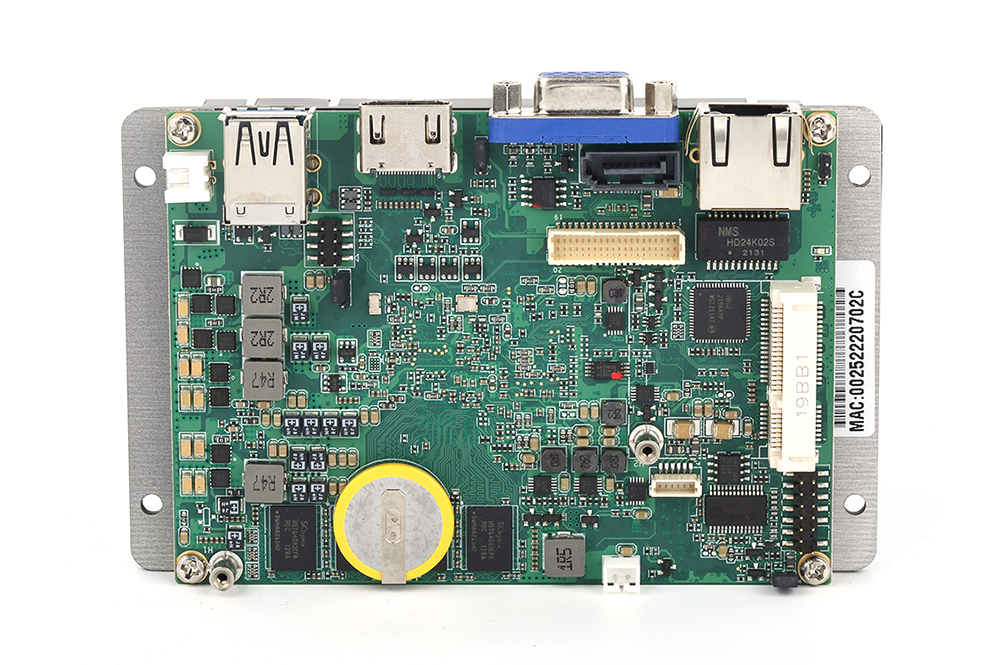
The industrial landscape in the United States is undergoing a profound digital transformation. Driven by the waves of Industry 4.0, smart manufacturing, and supply chain reshoring, American factories, warehouses, and energy facilities are rapidly upgrading their human-machine interfaces (HMIs) and display terminals. An Industrial PC Screen is no longer just a passive display monitor; it has evolved into an intelligent, rugged edge computing hub that processes complex data and controls critical operations in real-time.
From the heavy automotive assembly lines in the Midwest to the high-tech pharmaceutical cleanrooms in North Carolina and the demanding oil fields of Texas, the requirements for industrial displays are highly specialized. US system integrators and OEMs require hardware that guarantees 24/7 reliability under extreme conditions. This demands industrial-grade motherboards and SBCs that can withstand wide temperature fluctuations, severe vibrations, electromagnetic interference, and dust or moisture ingress.
SEO Insight for US Buyers: When sourcing industrial PC screens and embedded computing hardware, American engineers prioritize compliance, long-term product lifecycles (typically 5 to 10 years), NEMA/IP ratings for environmental protection, and robust technical support from experienced vendors.
Modern industrial screens are increasingly expected to perform localized data processing. With the integration of AI-driven predictive maintenance and machine vision on the factory floor, there is a growing demand for industrial motherboards equipped with high-performance processors, such as the Intel® Ultra and Tiger Lake-U series. These processors enable the HMI to run complex algorithms locally, reducing latency and bandwidth costs associated with cloud computing.
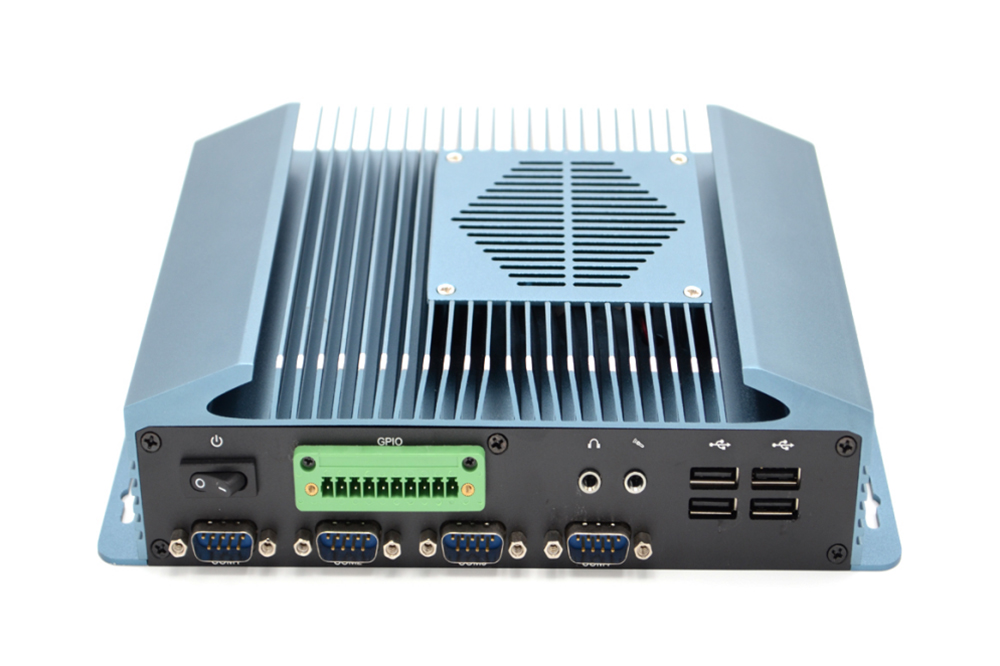
In dust-heavy environments like woodworking plants, metal fabrication facilities, and food processing units, cooling fans are often the primary point of failure. Fanless industrial PCs and HMI systems utilize passive cooling techniques, eliminating mechanical wear and tear. A fanless design prevents airborne contaminants from being sucked into the chassis, dramatically extending the operating lifespan of the system.
Many US applications—ranging from smart agriculture machinery and EV charging stations to oil pipelines and marine terminals—require outdoor installations. These environments expose the hardware to extreme cold in northern states like Minnesota and intense heat in southern states like Arizona. Industrial screens must be paired with wide-temperature motherboards (supporting -40°C to 85°C) and high-brightness displays to ensure readability under direct sunlight and stable operation in freezing conditions.
As factories transition to smart ecosystems, connectivity is key. Dual Gigabit or 2.5G Ethernet ports, multi-display outputs (such as HDMI, DisplayPort, and LVDS/eDP), and rich serial interfaces (RS-232/422/485) are standard requirements for US buyers. These allow the industrial PC screen to communicate simultaneously with PLCs, local networks, and legacy machinery.
Industrial PC screens and their underlying embedded systems find critical applications across various sectors in the United States. Below are some of the most prominent real-world use cases:
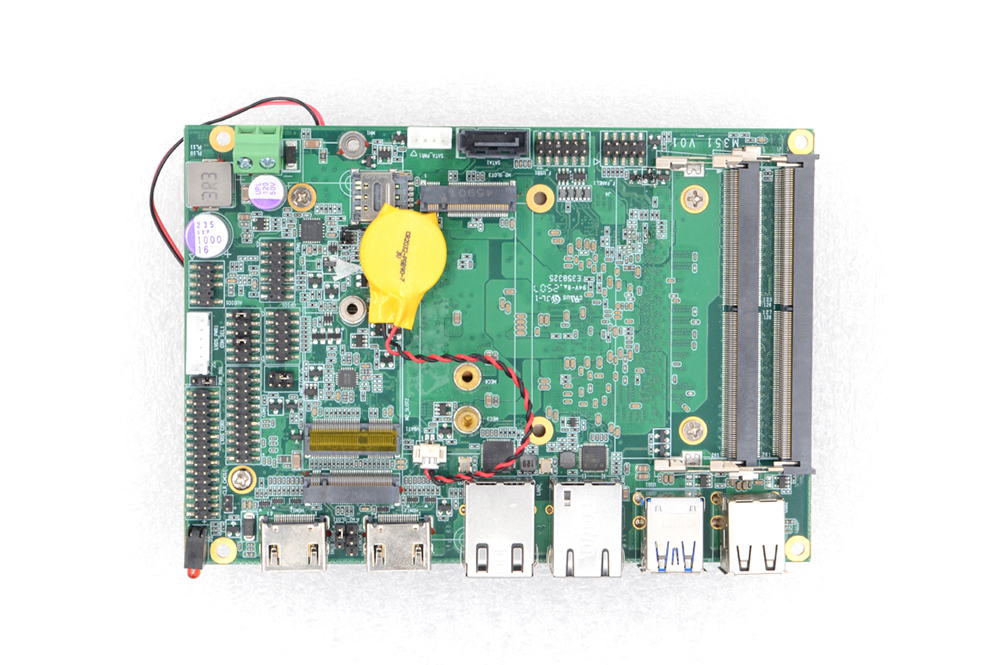
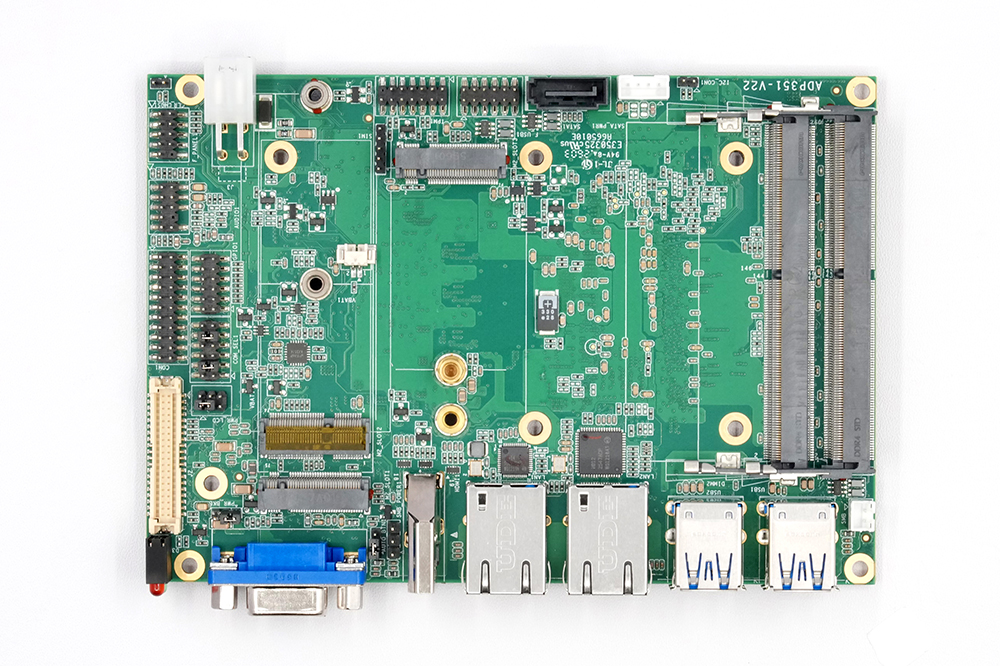
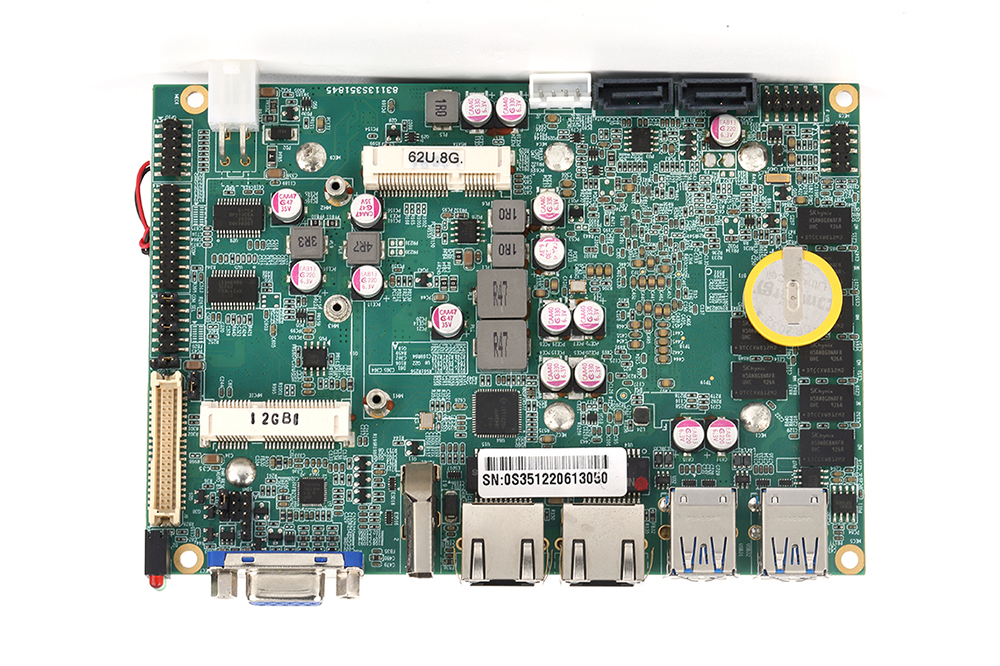
In major e-commerce fulfillment centers across the US, AGVs and Autonomous Mobile Robots (AMRs) navigate complex warehouse floors. These robots rely on compact, vibration-resistant 3.5-inch SBCs to process sensor data and render navigation maps on onboard touchscreens. Our industrial-grade mainboards provide the high shocking resistance and low power consumption required for continuous mobile operations.
The US healthcare sector demands the highest standards of precision and reliability. Diagnostic imaging machines, patient monitoring consoles, and laboratory automation equipment utilize fanless industrial motherboards to power high-definition touch displays. These boards must offer long-term availability, low electromagnetic radiation, and compliance with medical safety standards.
In the American energy sector, monitoring stations are often located in hazardous, remote areas. Outdoor terminal screens must operate reliably under extreme weather. Our wide-temperature motherboards with dual LAN ports ensure redundant, secure network connections, allowing operators to monitor pipeline pressure, power grids, and environmental metrics safely.
Food processing facilities require frequent cleaning with high-pressure, hot-water washdowns. Industrial screens used in these environments must be housed in stainless steel enclosures with IP66 or IP69K ratings. The internal computing boards must run cool without active ventilation, maintaining high performance inside airtight, sealed enclosures.
Shenzhen YDSTECH Electronics Co., Ltd. is a high-tech enterprise specializing in industrial computers. Since the establishment of YDSTECH in 1999, we have been committed to independent research and development, innovation, production and sales of industrial computers, and we own the independent intellectual property rights of our core products.
We consider honesty and pragmatism as our motto and make it our long-term goal to provide customers with cost-effective products. In order to achieve this goal, we work constantly to develop new products, improve our service capabilities and promote the innovation of embedded computer applications to create long-term value and potential growth for our customers.
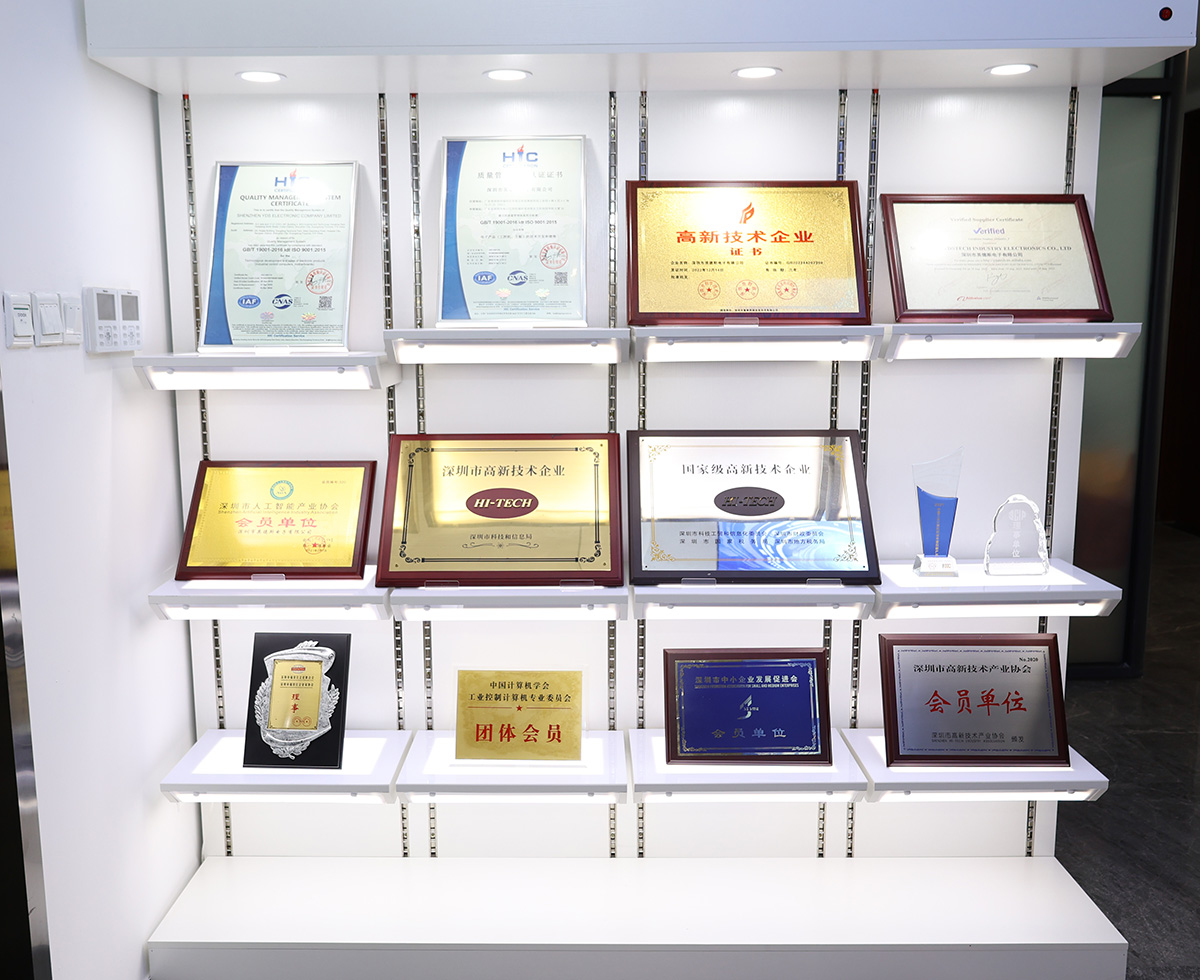
Our adherence to international quality standards guarantees that our products meet the strict regulatory requirements of the US and global markets.
Our core technical team has over 15 years of experience in this industry, and has been focusing on embedded computer research and development, with rich and solid professional expertise. We believe that attitude means everything, since the establishment of YDSTECH, we have always been committed to work with a conscientious, responsible, attentive, professional, prudent and meticulous attitude, which ensures the high-quality output of the products, years of persistence and experience created our strong R&D team.
For US system integrators requiring bespoke configurations, our R&D team offers extensive OEM/ODM services. Whether you need custom BIOS configurations, specific I/O layouts, specialized cooling mechanisms, or wide-voltage power modules, we deliver tailored solutions that fit seamlessly into your industrial screen enclosures.
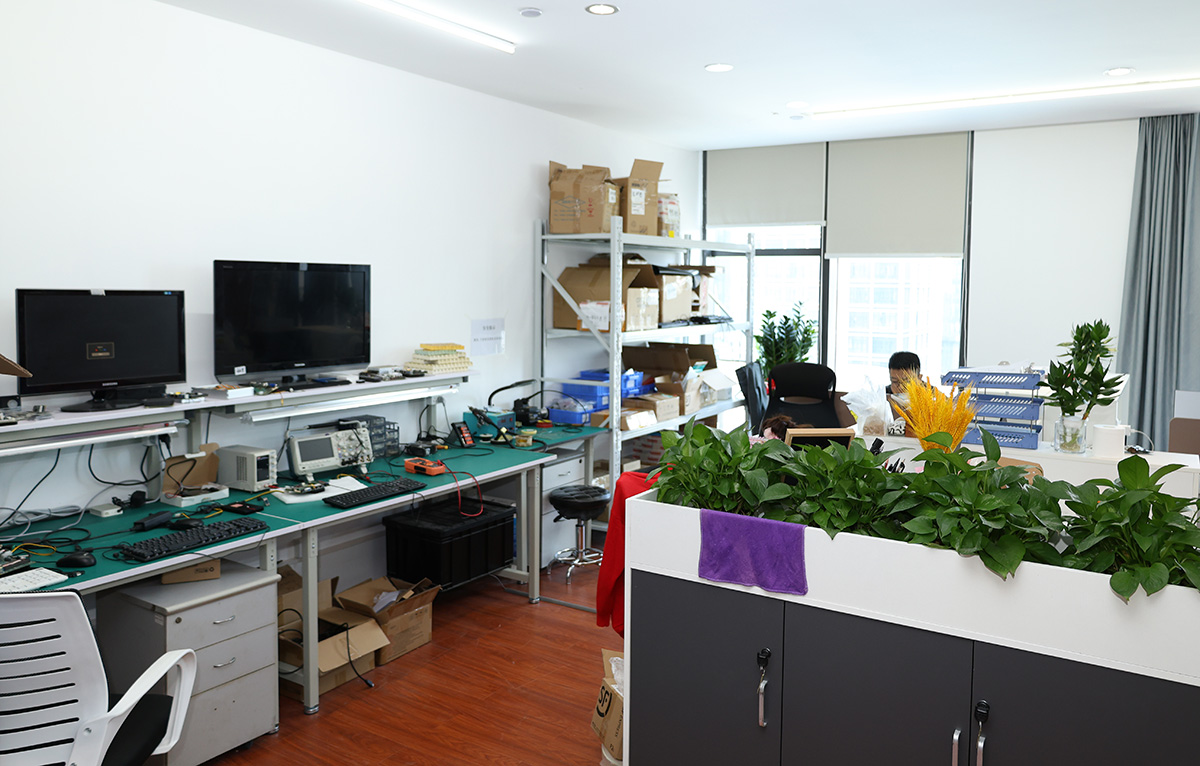
YDSTECH has set up a comprehensive quality assurance management system, adopting MSA quality system analysis, implementing rolling quality system audit, TQM, SPC process control and other quality management systems, establishing AVL supplier management system to ensure the quality of raw materials, and introducing rolling product reliability tests to ensure overall product reliability.
Every single board and controller undergoes rigorous thermal stress tests, vibration tests, and functional burn-in before leaving our facility, ensuring that when they reach our US clients, they deliver flawless performance in critical applications.
Select from our full catalog of high-reliability computing solutions optimized for industrial displays and rugged HMI applications in North America.