Leave Your Message
High-reliability embedded x86 computer hardware optimized for multi-channel RTD sensors, cleanroom HMI terminals, and automated qualification processes.
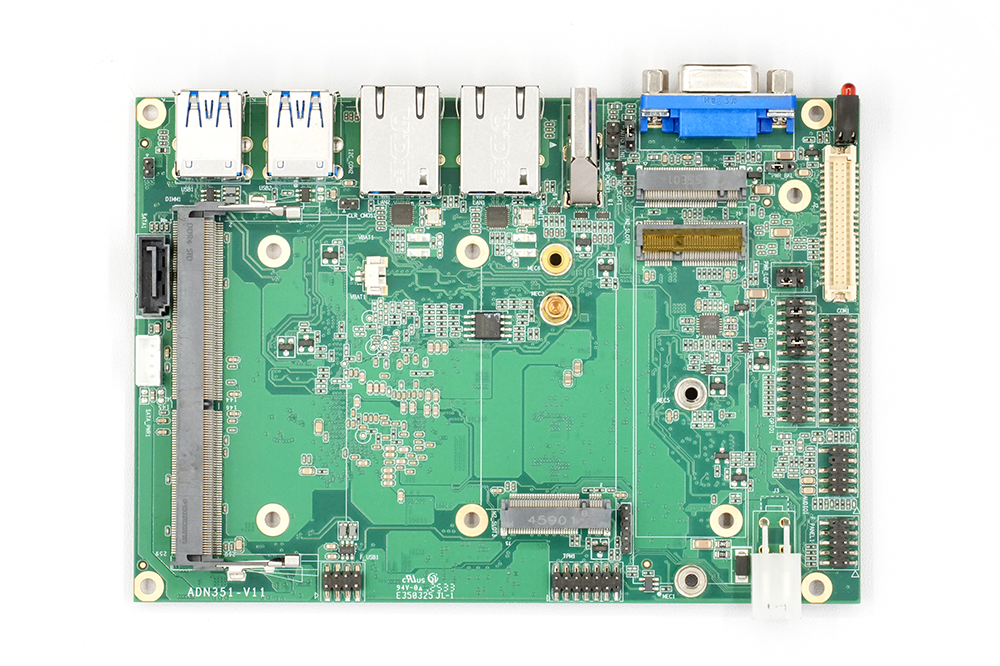
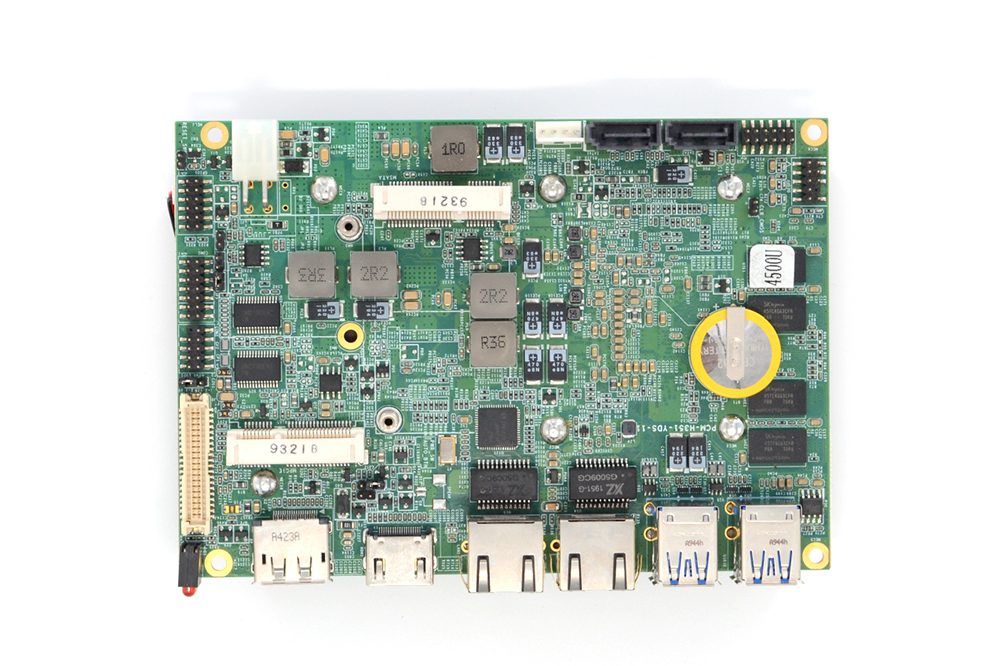
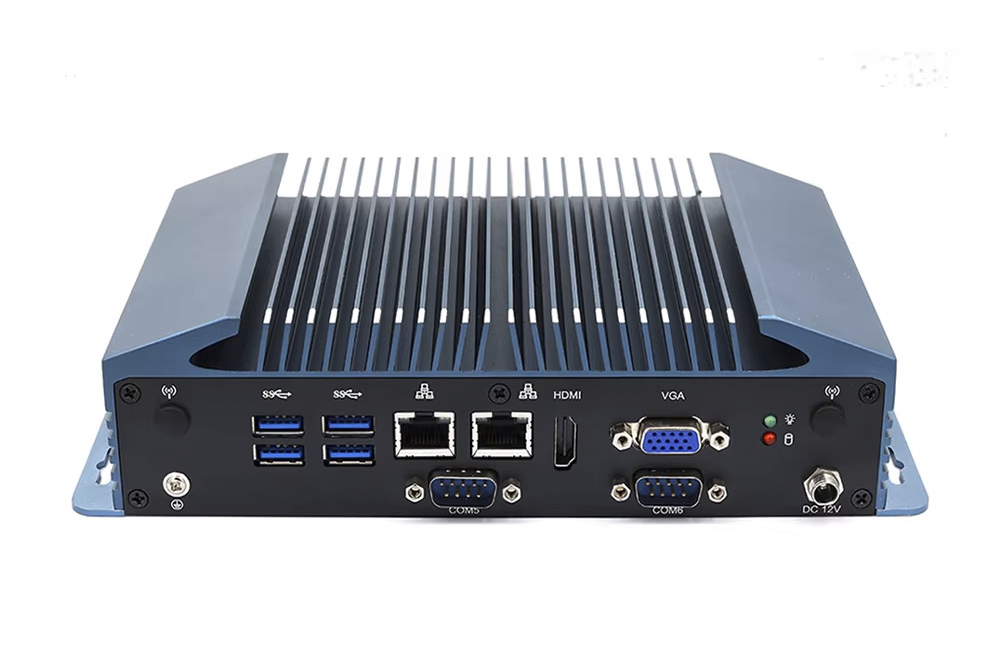
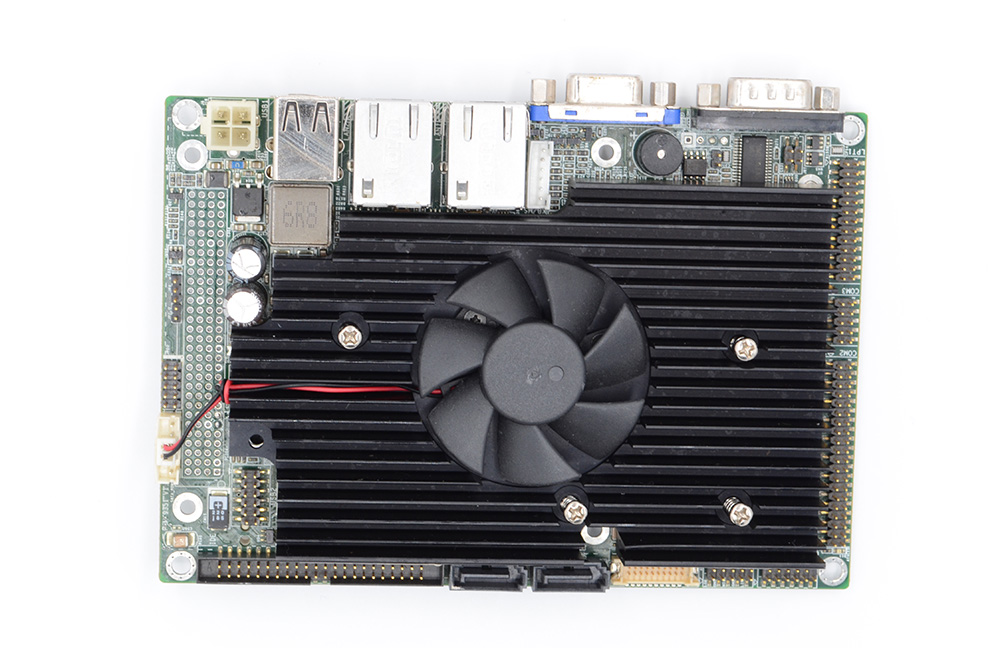
Ensuring absolute compliance with FDA 21 CFR Part 11, EU Annex 11, and strict cGMP thermal validation requirements.
In contemporary biopharmaceutical manufacturing and life science laboratories, temperature precision is non-negotiable. From active pharmaceutical ingredient (API) synthesis and bioreactor fermentation to cold chain vaccine storage and autoclave sterilization, strict thermal control dictates product efficacy, stability, and patient safety. Global regulatory frameworks, including FDA 21 CFR Part 11, EU GMP Annex 11, GAMP 5, and WHO Good Distribution Practices (GDP), mandate continuous data acquisition, uninterrupted audit trails, and strict ALCOA+ data integrity standards across all critical control points (CCPs).
To execute reliable thermal mapping, continuous environmental monitoring (CMS), and automated qualification (IQ/OQ/PQ), pharmaceutical facilities are increasingly replacing standard computing platforms with Industrial Fanless Panel PCs. The elimination of motorized cooling fans is vital: active fans generate micro-turbulences that disrupt laminar airflow in ISO Class 5 / Class A sterile cleanrooms and introduce particulate accumulation that violates particulate count limits. A completely sealed, passively cooled industrial panel PC ensures zero air agitation, seamless wipe-down capability with aggressive sanitizing agents (such as Spor-Klenz, Isopropyl Alcohol, and Hydrogen Peroxide vapors), and exceptional thermal endurance across -40°C to +75°C.
ALCOA+ Compliance Guarantee: Industrial Fanless Panel PCs integrated with hardware-level TPM 2.0 security, dual watchdog timers, and non-volatile NVMe storage ensure that all temperature data points remain Attributable, Legible, Contemporaneous, Original, and Accurate without risk of lost validation packets during sudden power transients.
Full IP65/IP66/IP69K stainless steel or aluminum die-cast front bezels resist regular high-pressure washdowns, corrosive chemical disinfectants, and vaporized hydrogen peroxide (VHP) decontamination cycles without ingress or material degradation.
Engineered to operate seamlessly across an extreme thermal envelope of -40°C to +75°C, ensuring reliable operation directly alongside ultra-low temperature (ULT) cryogenic freezers (-86°C) as well as heat-intensive steam sterilization autoclaves (+134°C).
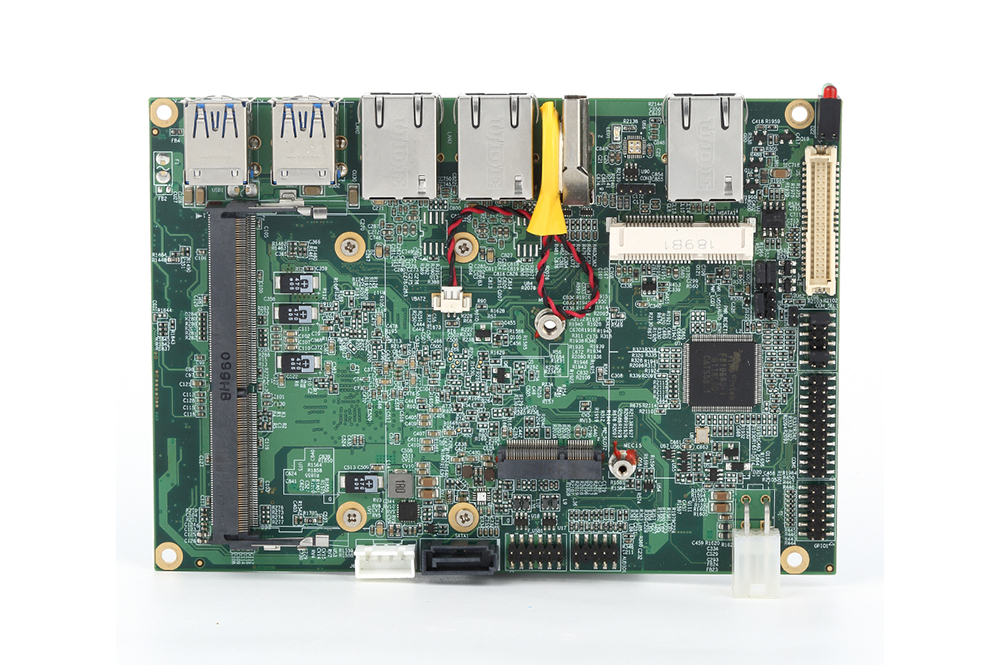
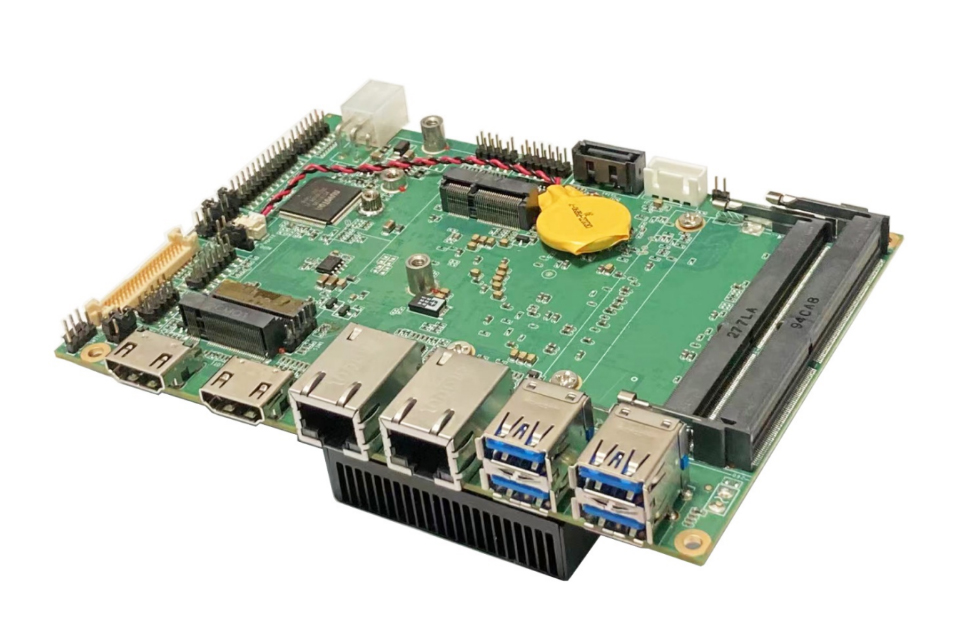
Rich isolated I/O interfaces including dual Intel Gigabit Ethernet, multiple RS485/Modbus RTU ports, and GPIO facilitate direct connectivity to 64+ Pt100/Pt1000 RTD temperature sensors, humidity transmitters, and differential pressure sensors.
Comprehensive mission-critical deployment models across production, sterilization, storage, and cleanroom environments.
Sterilization processes utilizing moist heat autoclaves (typically operating between 121°C and 134°C) and freeze-drying lyophilizers require meticulous temperature validation to calculate F0 lethal rates and ensure absolute pathogen elimination. Industrial Fanless Panel PCs act as the core HMI and edge computing hub for multichannel thermocouple and wireless data logger matrices. Because fanless panel PCs produce zero mechanical vibration, internal solid-state components remain immune to the acoustic vibrations and mechanical shocks often generated by heavy autoclave vacuum pumps.
Cleanrooms classified under ISO 14644-1 require round-the-clock surveillance of room temperature, relative humidity, airborne particle counts, and differential air pressure. Industrial Panel PCs mounted flush on cleanroom walls act as local visualization terminals. The optical bonding multi-touch screens allow operators wearing double latex or nitrile gloves to interact seamlessly with supervisory SCADA interfaces. In case of unexpected temperature excursion outside validated setpoints (e.g., 20°C to 24°C ± 0.5°C), the fanless system instantly triggers optical/acoustic alarm relays and automatically transmits encrypted alerts to the centralized BMS/LIMS networks.
Modern cell and gene therapy (CGT) formulations and mRNA-based vaccines require ultra-cold storage between -80°C and -196°C in liquid nitrogen vapor phase freezers. Industrial fanless computers equipped with wide-temperature motherboards (-40°C to +75°C) guarantee that external HMI stations mounted in chilly cold-room anterooms remain fully operational without boot failures, cold-start latency, or LCD screen crystallization. Dual Gigabit Ethernet ports allow redundant network uplinks, guaranteeing continuous validation data logging even if primary Ethernet lines suffer hardware disruption.
How next-generation x86 embedded computing is evolving pharmaceutical manufacturing quality control.
The pharmaceutical sector is undergoing a rapid digital shift toward Pharma 4.0, characterized by the integration of edge computing, artificial intelligence (AI), and real-time release testing (RTRT). Rather than relying solely on retrospective validation reports generated days after a batch is finished, pharmaceutical manufacturers are employing Industrial Fanless Panel PCs powered by 12th/13th Generation Intel Core and Tiger Lake-U processors to execute dynamic thermal modeling and predictive drift analytics right at the manufacturing line.
Onboard machine learning algorithms analyze thousands of historical temperature micro-fluctuations in real-time, detecting thermocouple calibration drift and insulation degradation before a batch suffers irreversible temperature deviations.
Dual isolated Gigabit LAN interfaces provide strict physical segmentation between sensitive cleanroom OT machinery and enterprise IT/Cloud systems, ensuring real-time telemetry streaming with zero malware exposure.
High-speed DDR4 memory (up to 64GB) and powerful multi-core processing simulate exact thermodynamic air distributions inside cleanrooms and cold warehouses, enabling virtual spatial mapping and rapid re-qualification.
Pioneering independent R&D and high-reliability industrial embedded computer manufacturing since 1999.
Shenzhen YDSTECH Electronics Co., Ltd. is a high-tech enterprise specializing in industrial computers. Since the establishment of YDSTECH in 1999, we have been committed to independent research and development, innovation, production and sales of industrial computers, and we own the independent intellectual property rights of our core products.
We consider honesty and pragmatism as our motto and make it our long-term goal to provide customers with cost-effective products. In order to achieve this goal, we work constantly to develop new products, improve our service capabilities and promote the innovation of embedded computer applications to create long-term value and potential growth for our customers.
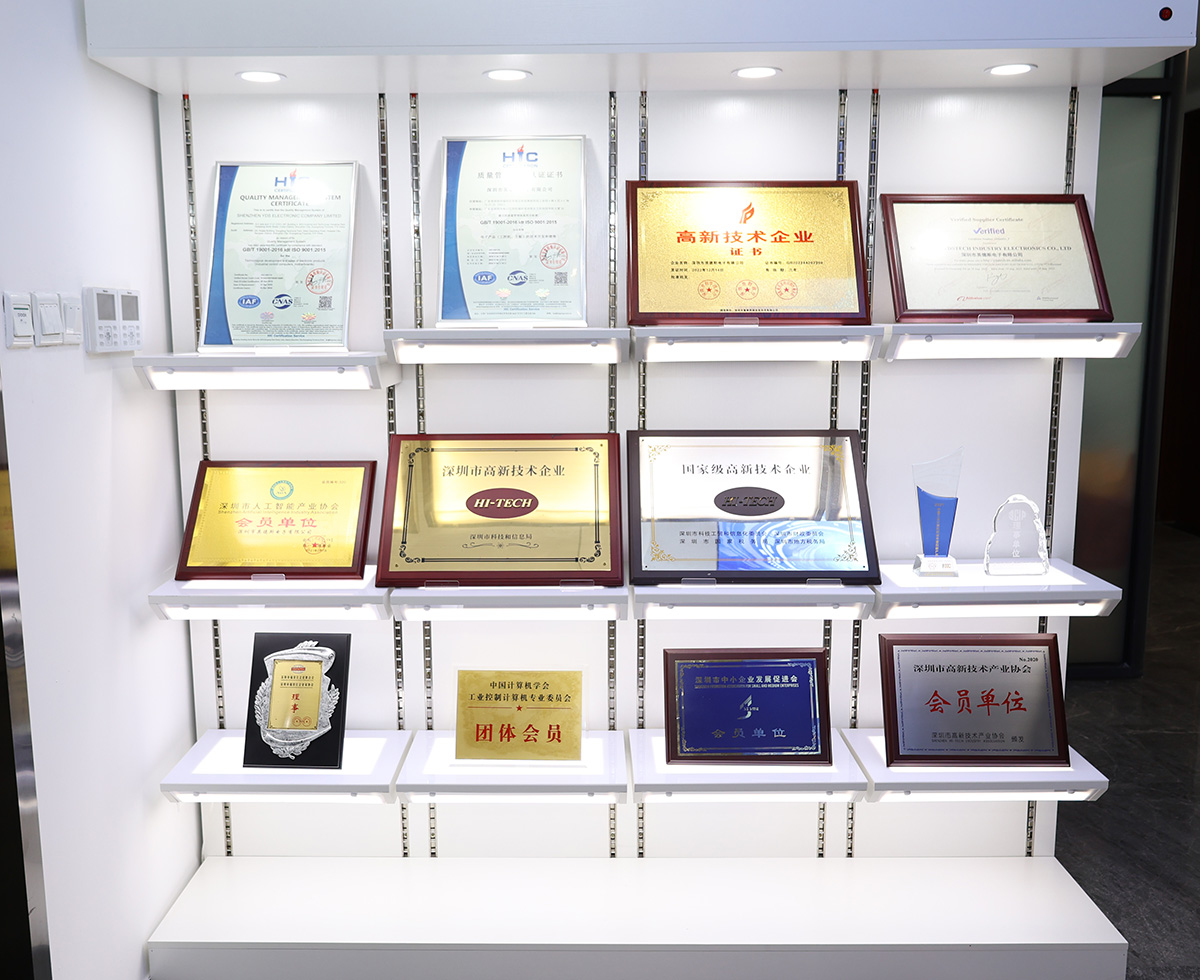
Adhering strictly to international manufacturing standards and industry compliance benchmarks:
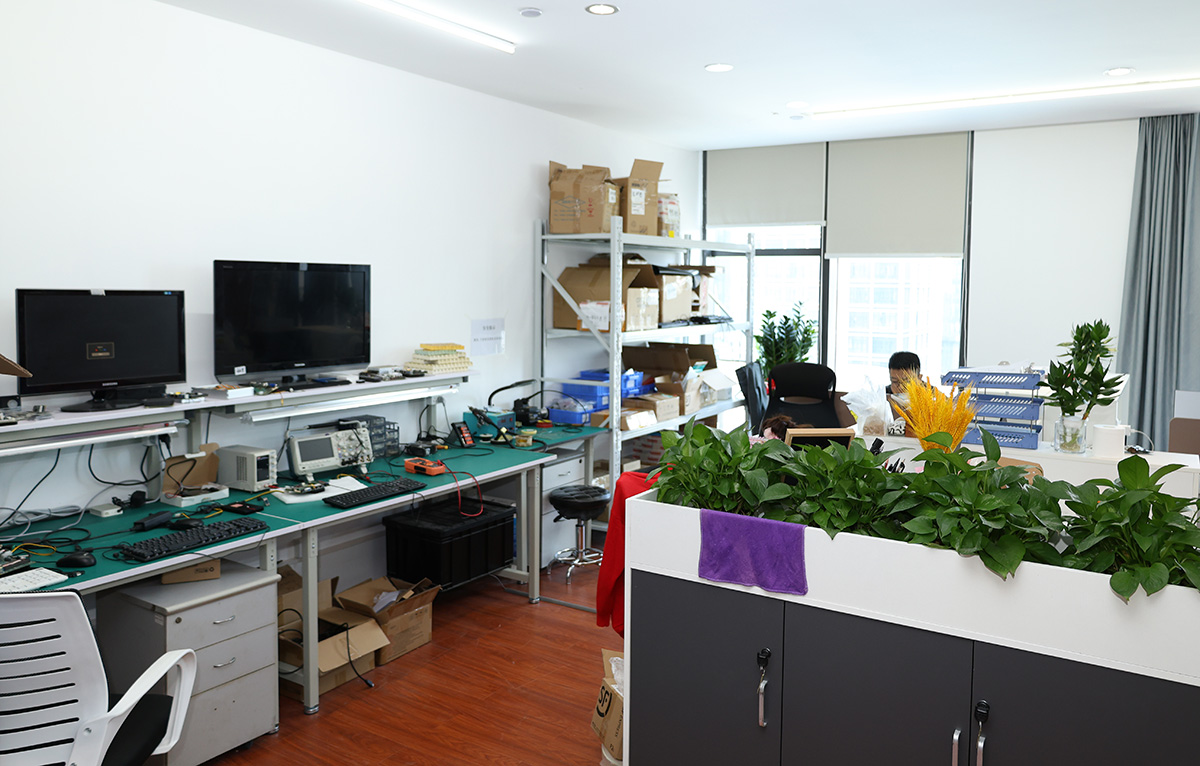
Our core technical team has over 15 years of experience in this industry, and has been focusing on embedded computer research and development, with rich and solid professional expertise. We believe that attitude means everything, since the establishment of YDSTECH, we have always been committed to work with a conscientious, responsible, attentive, professional, prudent and meticulous attitude, which ensures the high-quality output of the products, years of persistence and experience created our strong R&D team.
YDSTECH has set up a comprehensive quality assurance management system, adopting MSA quality system analysis, implementing rolling quality system audit, TQM, SPC process control and other quality management systems, establishing AVL supplier management system to ensure the quality of raw materials, and introducing rolling product reliability tests to ensure overall product reliability.
Explore our complete range of wide-temperature x86 motherboards, compact SBCs, and fanless industrial computers designed for medical, pharmaceutical, and automation validation environments.