


Leave Your Message
High-performance, reliable, and wide-temperature embedded motherboards designed to meet the rigorous compliance standards of the United States medical and healthcare device sectors.
The United States represents the largest medical device market in the world, accounting for over 40% of the global market share. With major healthcare hubs in Texas, California, Massachusetts, and Minnesota, US medical OEMs (Original Equipment Manufacturers) demand the highest standards of reliability, longevity, and regulatory compliance for embedded computing systems.
Medical equipment motherboards serve as the computational core for critical devices, including diagnostic imaging (MRI, CT, ultrasound), patient monitoring systems, clinical laboratory analyzers, and surgical robotics. Unlike consumer-grade electronics, medical-grade motherboards must undergo rigorous validation processes to comply with FDA regulations and ensure patient safety in hospital environments.
Motherboards destined for US medical devices must meet strict electromagnetic compatibility (EMC) guidelines to prevent interference with sensitive clinical equipment, aligning with UL 60601-1 safety standards.
US healthcare providers require equipment with long operational lifespans. Vendors must guarantee component longevity to avoid frequent and costly FDA re-certifications.
Any change in motherboard components can trigger a regulatory review. Rigid revision lock is mandatory for medical device manufacturers operating in the US.
To protect both patients and operators, medical-grade motherboards often feature isolated COM ports, LAN ports, and USB interfaces to block electrical surges.
Modern diagnostic devices require real-time data processing. The integration of high-performance CPUs, such as Intel Ultra U/H series, enables edge artificial intelligence directly on the motherboard, allowing for faster diagnostics in oncology, cardiology, and radiology.
In sterile environments like operating rooms and intensive care units (ICUs), fanless designs are critical. They prevent the circulation of airborne pathogens and dust, while ensuring silent operation that reduces ambient noise for patients and medical staff.
With the rise of mobile clinics and emergency response vehicles (EMS) across the United States, embedded motherboards must operate reliably in extreme environments, supporting temperature ranges from -40°C up to +85°C.
Medical imaging displays require massive data throughput. Motherboards featuring dual 2.5G/10G Ethernet ports, multi-display outputs (HDMI/DP/eDP), and high-speed DDR5 memory are becoming the industry standard for modern US medical devices.
Embedded motherboards are deployed across a wide array of localized healthcare applications throughout the United States, proving their durability and high-performance computing capabilities daily:
In major medical centers in Houston and Boston, high-performance x86 motherboards power ultrasound machines and CT scanners, processing complex 3D rendering and imaging data with minimal latency.
In intensive care units (ICUs) across New York hospitals, fanless 3.5-inch and 2.5-inch motherboards run continuously, tracking patient vitals and securely transmitting data to centralized nursing stations.
Biotech research labs in California rely on embedded motherboards with multiple serial ports and dual gigabit Ethernet to automate blood analysis, genetic sequencing, and chemical screening processes.
First responders in the Midwest utilize rugged, wide-temperature motherboards inside emergency vehicles to maintain critical diagnostic and communication links under extreme physical shock and temperature swings.
When sourcing medical equipment motherboards for the US market, price is closely linked to the complexity of the design, the quality of the components, and the level of customization required. Standard industrial-grade motherboards can range from $150 to $500, while highly customized boards with advanced processors, medical certifications, and guaranteed 10-year lifecycles can range from $500 to over $1,500 per unit depending on order volume.
To optimize procurement costs, US medical device manufacturers partner with established vendors capable of providing prototype development, custom BIOS modifications, and comprehensive Quality Assurance (QA) certifications.
Shenzhen YDSTECH Electronics Co., Ltd. is a high-tech enterprise specializing in industrial computers. Since the establishment of YDSTECH in 1999, we have been committed to independent research and development, innovation, production and sales of industrial computers, and we own the independent intellectual property rights of our core products.
We consider honesty and pragmatism as our motto and make it our long-term goal to provide customers with cost-effective products. In order to achieve this goal, we work constantly to develop new products, improve our service capabilities and promote the innovation of embedded computer applications to create long-term value and potential growth for our customers.
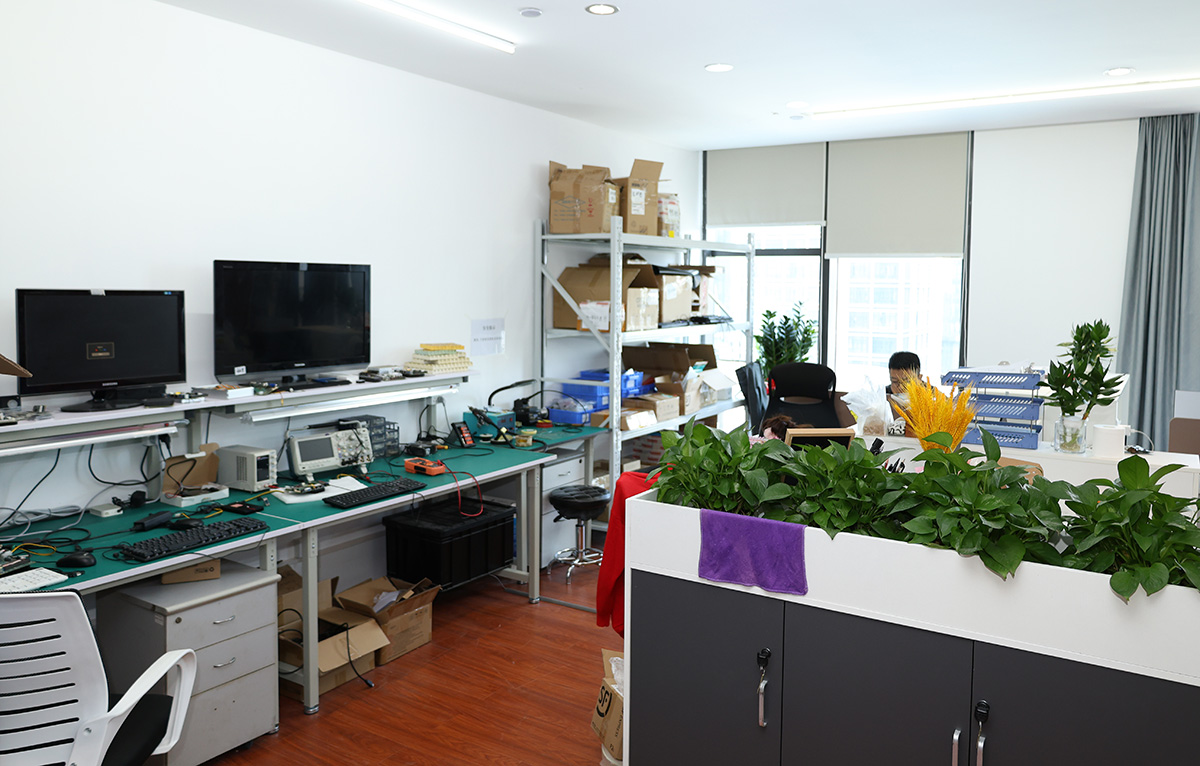
Our core technical team has over 15 years of experience in this industry, and has been focusing on embedded computer research and development, with rich and solid professional expertise. We believe that attitude means everything, since the establishment of YDSTECH, we have always been committed to work with a conscientious, responsible, attentive, professional, prudent and meticulous attitude, which ensures the high-quality output of the products, years of persistence and experience created our strong R&D team.
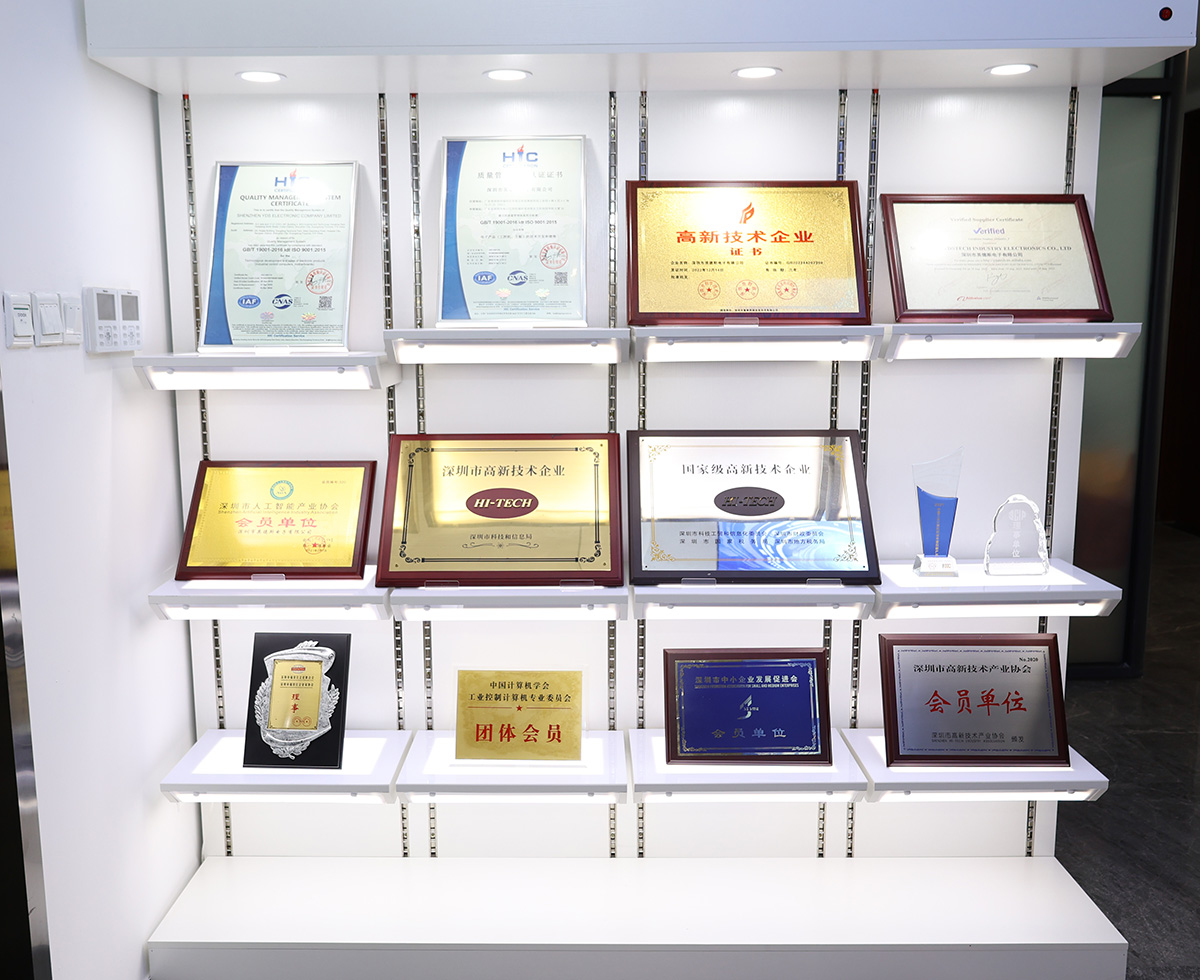
YDSTECH has set up a comprehensive quality assurance management system, adopting MSA quality system analysis, implementing rolling quality system audit, TQM, SPC process control and other quality management systems, establishing AVL supplier management system to ensure the quality of raw materials, and introducing rolling product reliability tests to ensure overall product reliability.
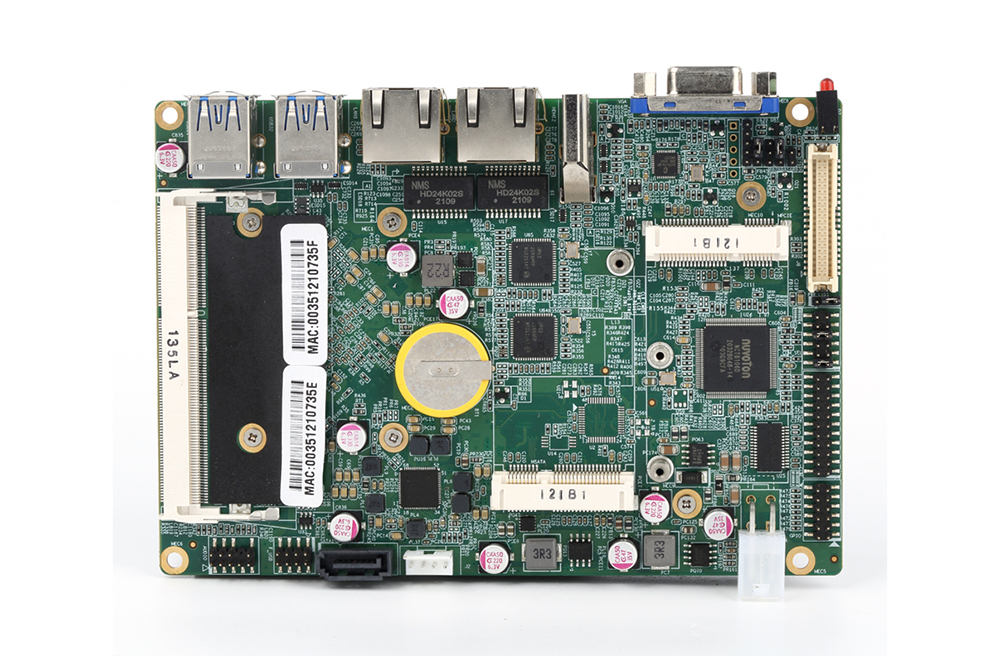 3.5 inch Wide Temp Range Embedded Industrial Motherboard
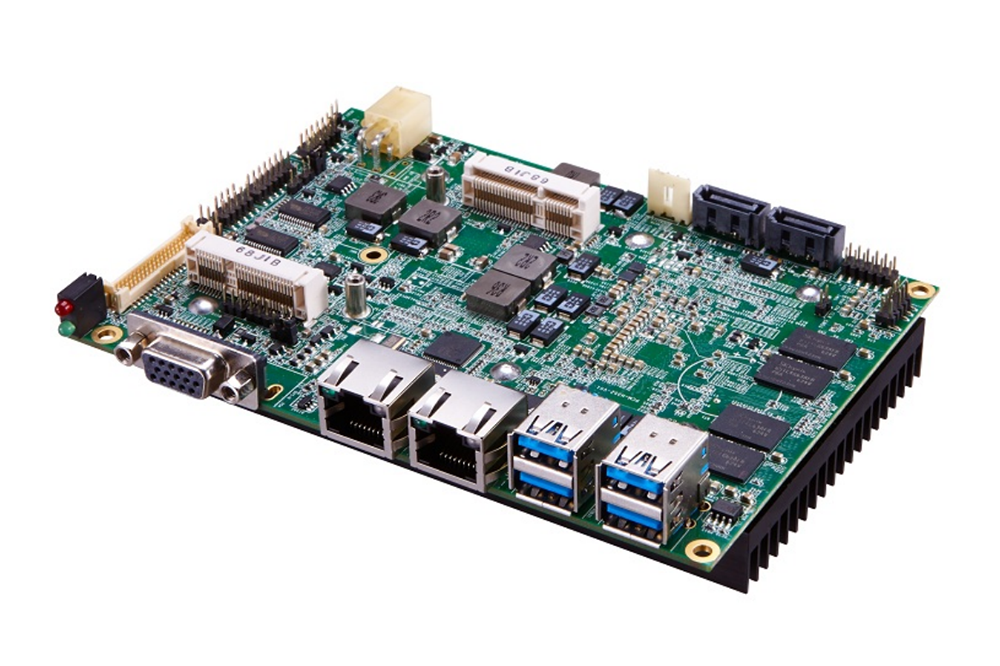 Fanless X86 Embedded IPC Motherboard
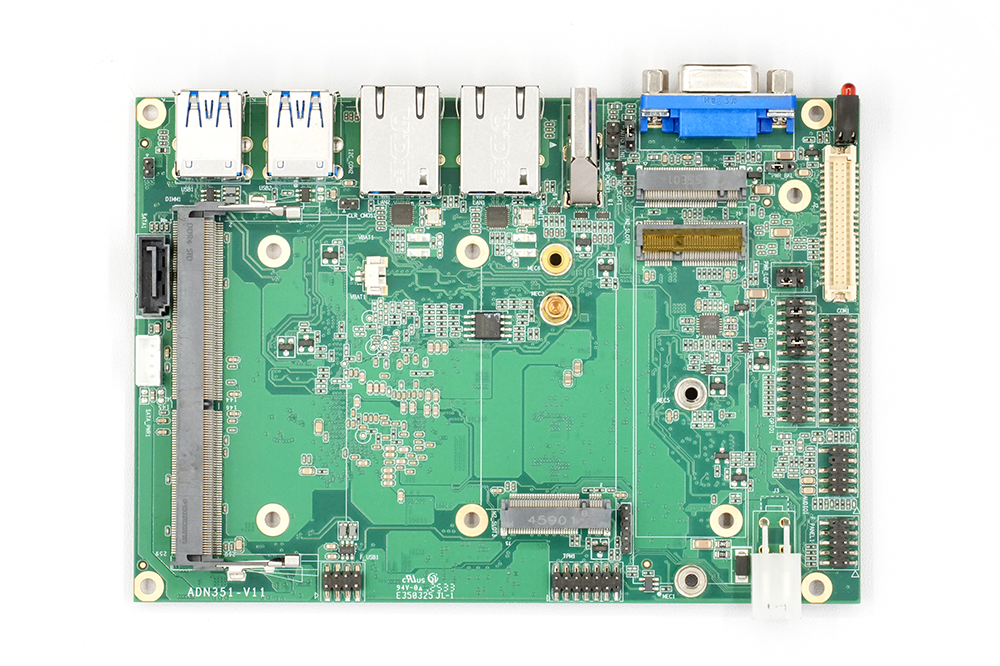 Industrial-Grade X86 3.5 Inch Motherboard, Wide Temperature -40℃~+75℃
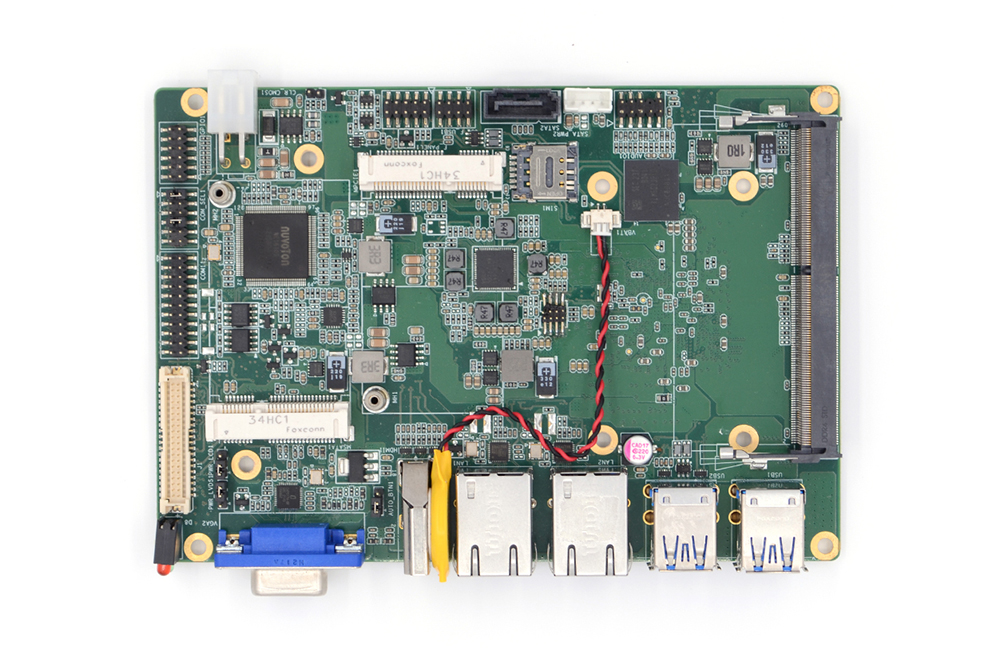 3.5" X86 Embedded PC Motherboard -40℃~+85℃ Wide-Temp with Dual Gigabit Ethernet & Multi-Serial Ports
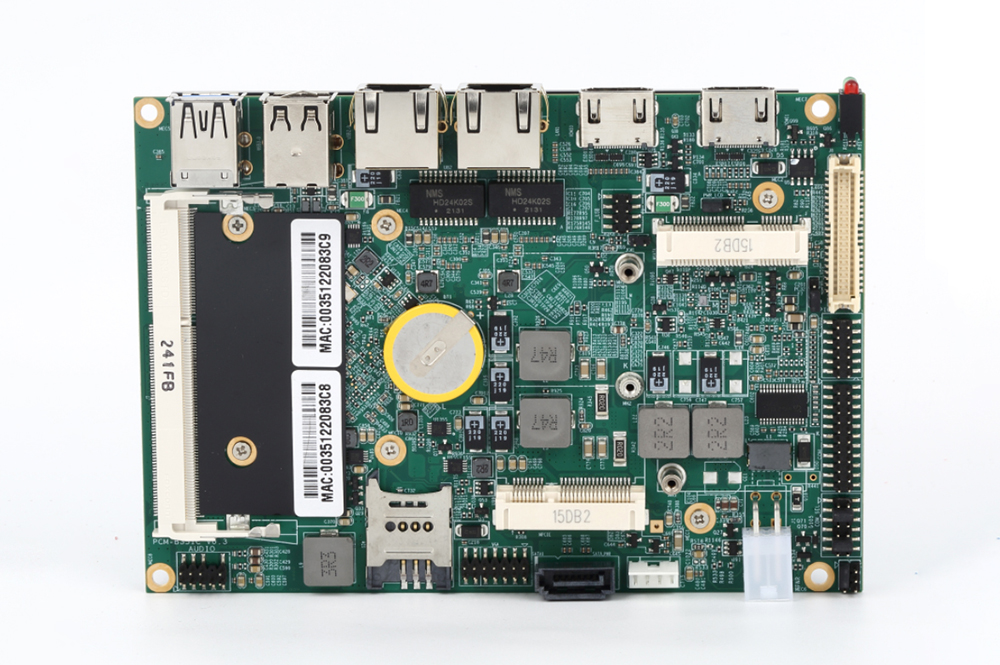 Fanless 3.5 Inch X86 Industrial Motherboard with Baytrail Atom/Celeron SOC
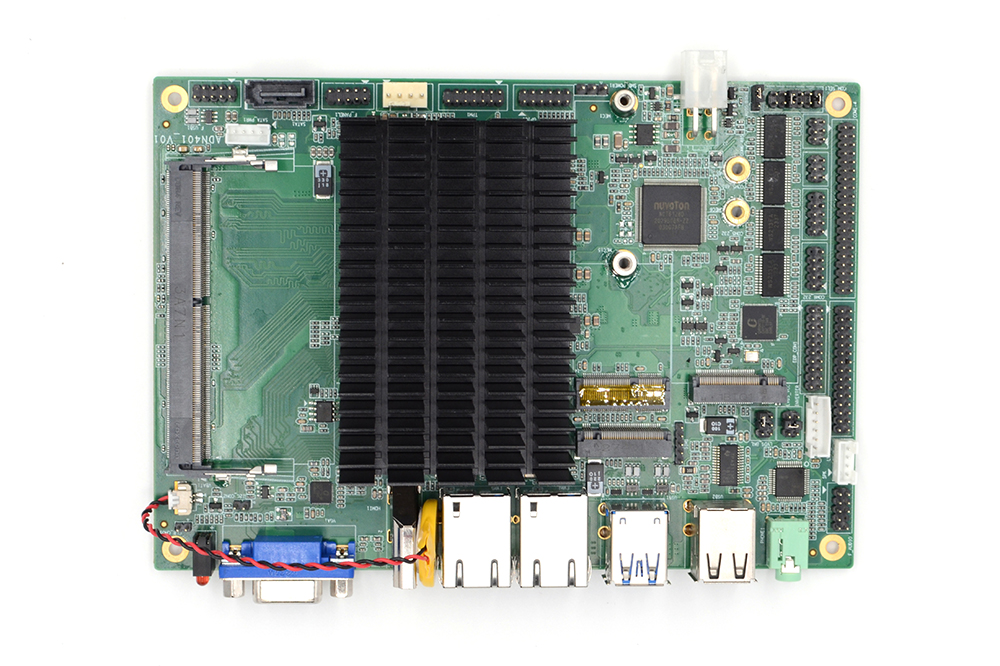 4 Inch X86 Industrial Motherboard Wide Temp Operation, Intel Low Power CPU Up to 32GB DDR4 Dual LAN Multi Video Output
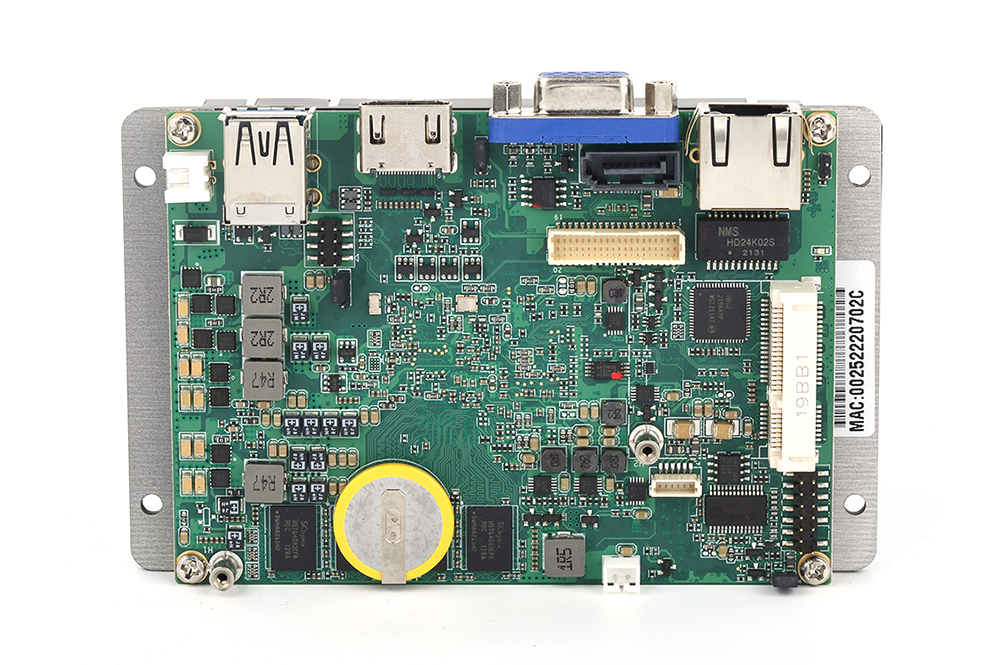 2.5 Inch Intel x86 Fanless Industrial Motherboard
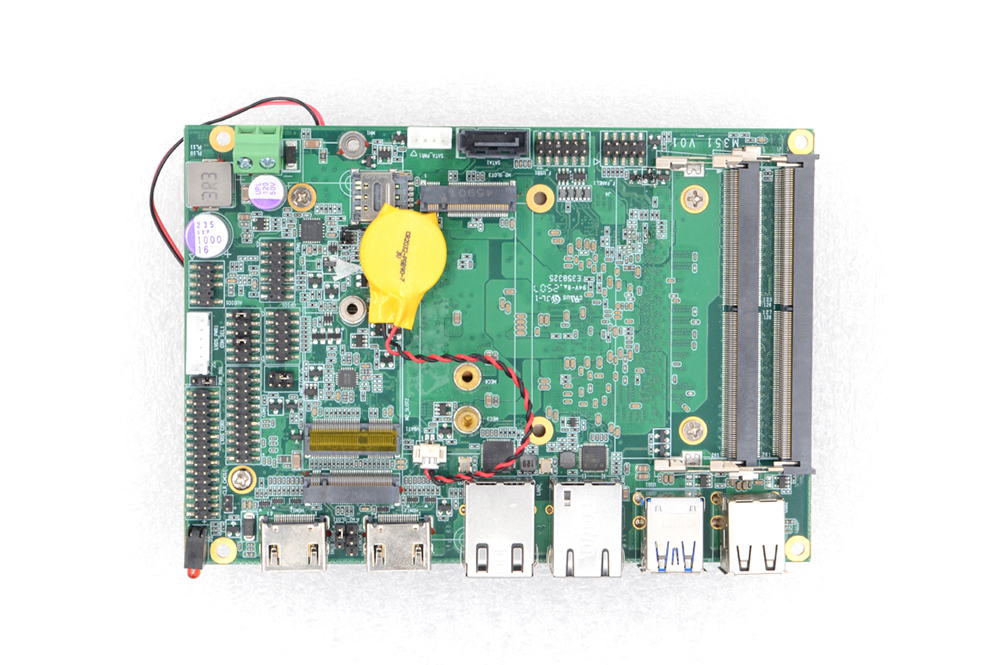 Wide Temp X86 Industrial Motherboard, Intel Ultra U/H CPU, Up to 64GB DDR5, Multi-Display & Dual 2.5G Ethernet Ports